Factory Direct Commercial LED Backlight Catalog
Engineered for commercial fitouts, translucent stone backlighting, custom joinery, and architectural linear lighting across Auckland, Wellington, Christchurch, and regional NZ.
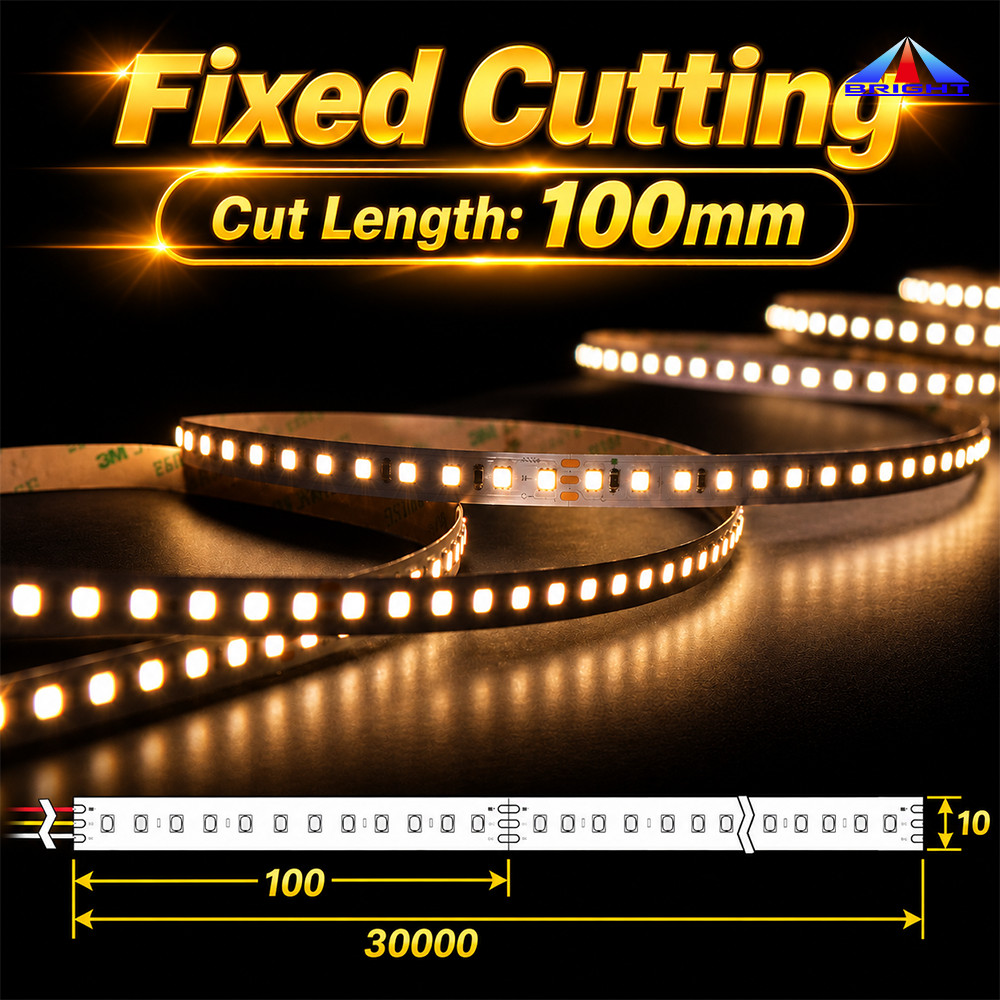
2835 Dual Color CCT Flexible LED Strip DC48V Double-sided FPC 2700K-6500K
WiFi LED Strip Light SMD2835 Cuttable Flexible Tape 2200K-6500K DC12V IP20
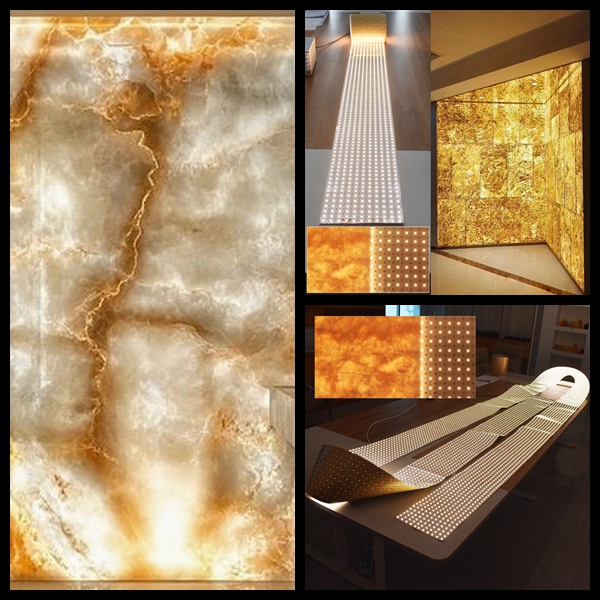
DC24V 10M Ultra Long Flexible SMD2835 LED Sheet Panel 528 LEDs CRI 90
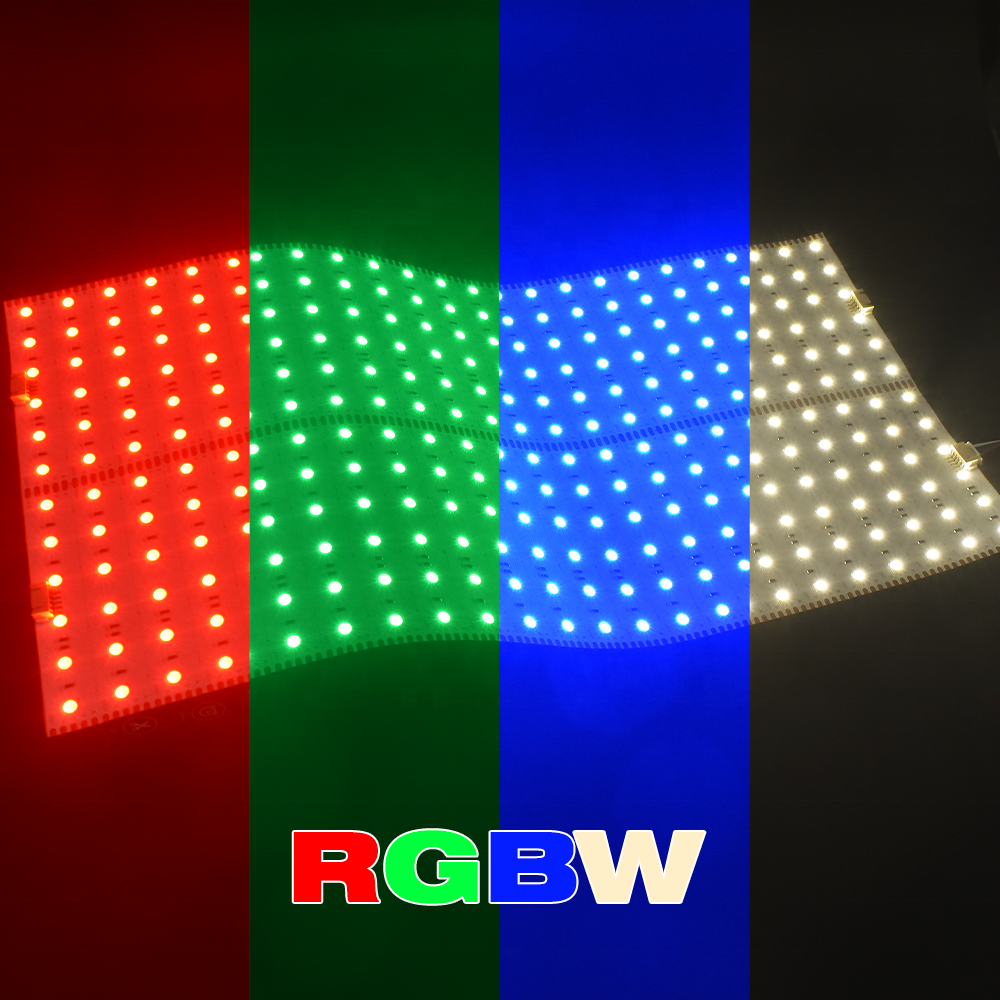
CE RoHS RGBW LED Light Sheet Backlight Panel IP54 DC24V for Translucent Stone
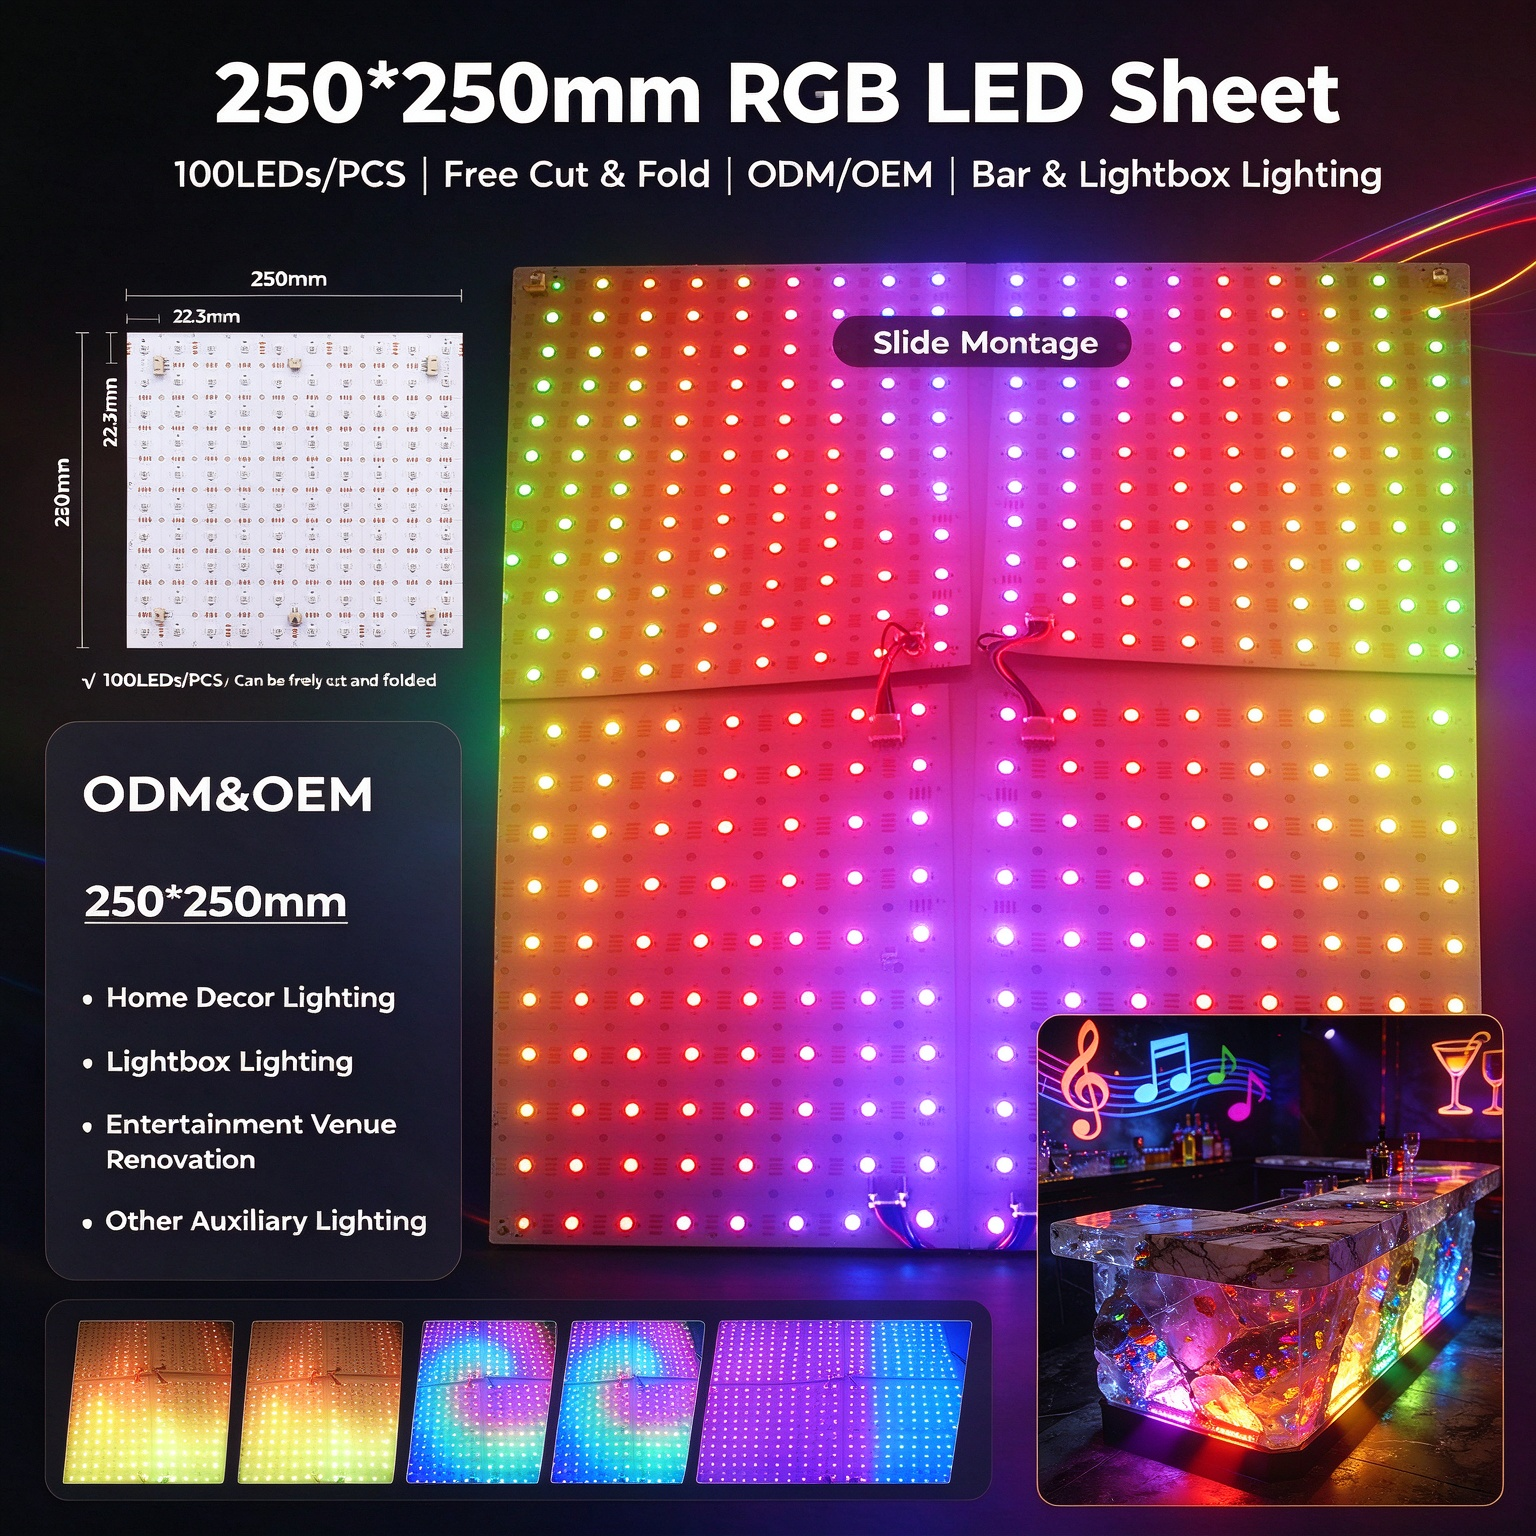
RGB Digital LED Sheet Panel DC 12V SMD5050 100 LEDs 100 Pixels Cuttable
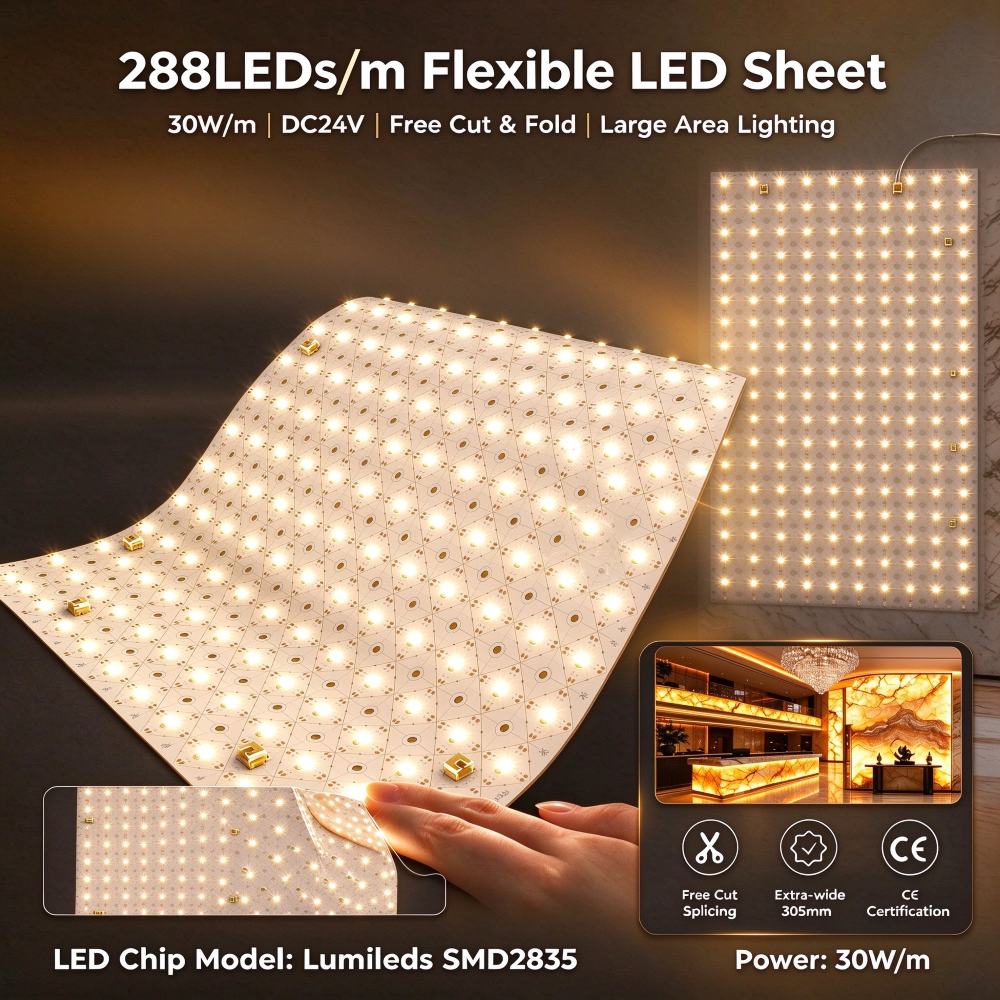
Flexible 610*305mm LED Backlighting Panel Light DC24V 288 LEDs 2700K-6000K
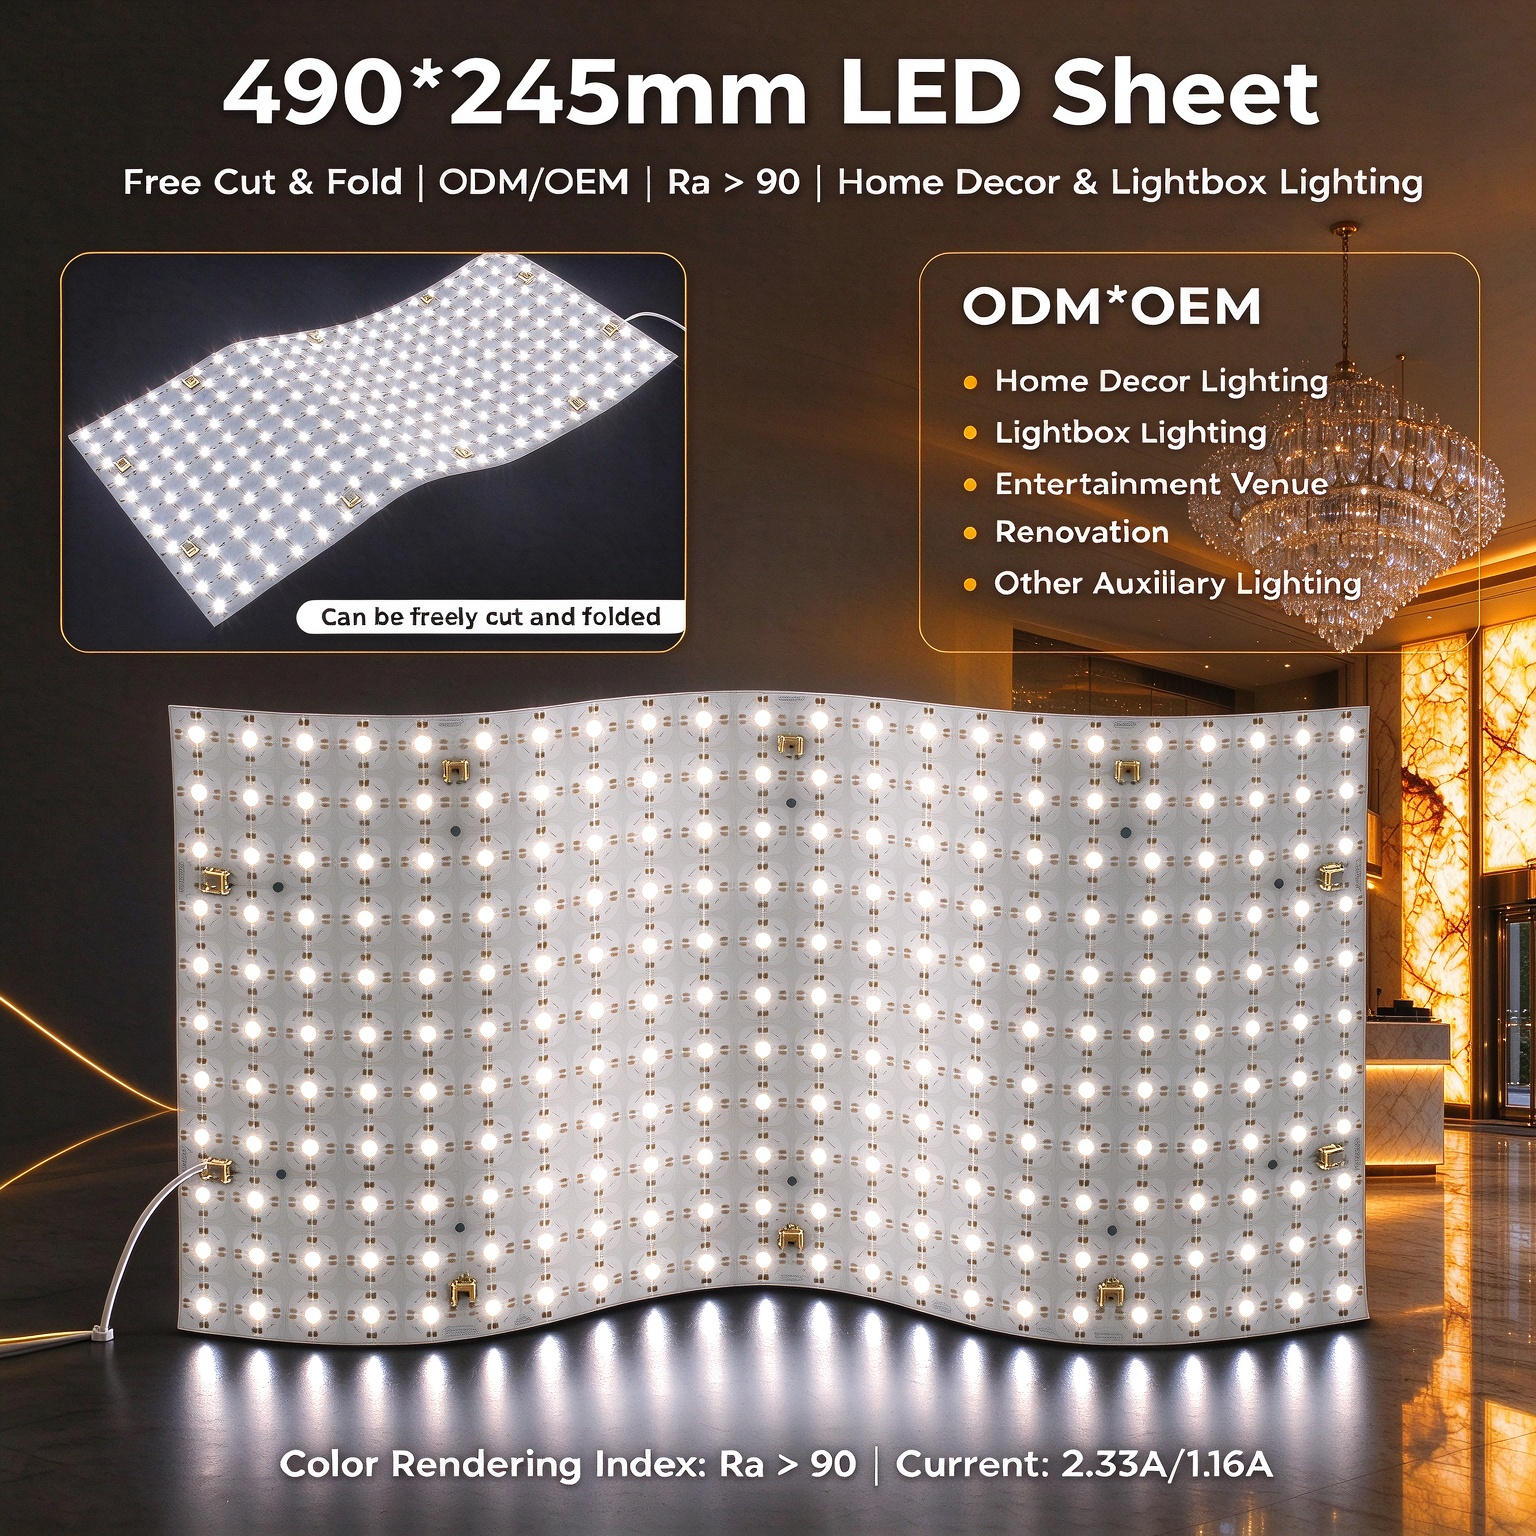
242 LEDs Flexible Sheet Panel Light DC24V 28W Cuttable Backlight 490 X 245mm
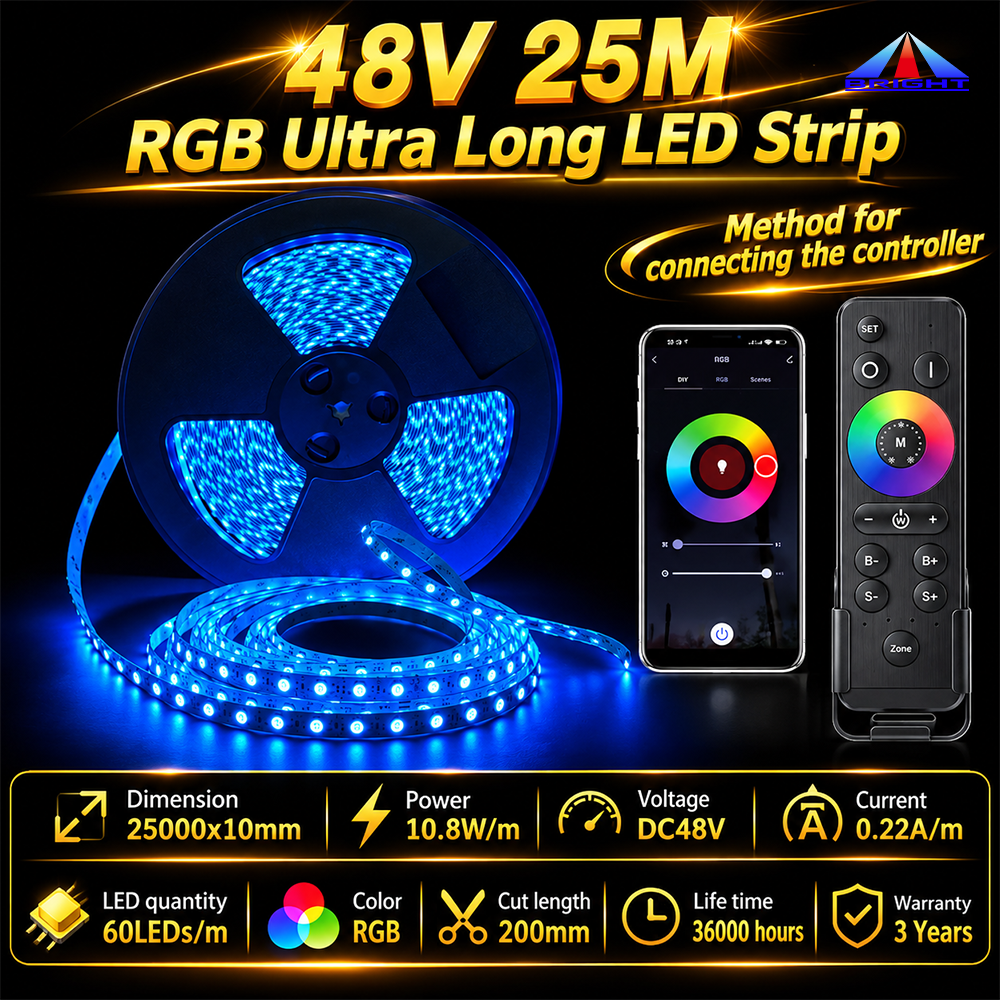
DC48V Durable RGB SMD Flexible LED Strip Light High Brightness for Bar & Pool Decor
State of Architectural Backlighting in New Zealand: Market Trends & Intent Mining
The New Zealand commercial architectural sector—led by urban expansions in Auckland CBD, Newmarket, Wellington Waterfront, and Queenstown hospitality hubs—is undergoing a structural shift toward integrated linear illumination and translucent solid-surface backlighting. Traditional rigid fluorescent boxes and bulky edge-lit aluminum frames are being rapidly replaced by high-density, matrix-cuttable flexible LED backlight sheets and ultra-narrow COB (Chip-on-Board) LED strips.
Local electrical wholesalers, stone masons, and commercial lighting contractors face distinct geographic and environmental conditions in Aotearoa New Zealand:
Seismic Resilience & Flex Dynamics
Structural movements engineered into NZ modern building codes require lighting components behind stonework or glass to flex without mechanical fatigue. Flexible PCB backlights absorb vibration and avoid micro-fractures in solder joints.
Low-Glare & Biophilic Design
Luxury residential lodges in Wanaka and boutique hotels in Auckland emphasize natural timber and translucent natural stones (such as Coromandel granite, imported Italian onyx, and engineered quartz). Dotless backlighting eliminates distracting hotspots.
Strict AS/NZS Compliance Requirements
Electrical safety and electromagnetic compatibility are strictly enforced. Importers require low-voltage DC24V and DC48V Class 2 certified modules that comply with AS/NZS 60598.2.21 and AS/NZS 3000 Wiring Rules.
As a specialized OEM/ODM manufacturer, Shenzhen Covek Lighting Co., Ltd. bridges the gap between China’s advanced LED semiconductor packaging and New Zealand’s high-precision architectural fitouts. By delivering high lumen-per-watt efficiency, strict MacAdam 3-Step color binning, and customizable cutting grids, we empower local NZ distributors and lighting designers to achieve uncompromised visual aesthetics.
OEM/ODM Technical Specifications & Voltage Engineering Guide
To prevent thermal decay and visible voltage drop across long continuous runs in large-scale installations (such as hotel lobbies, airport retail, or multi-level shopping centers), understanding the physics of copper trace weight and electrical pressure is paramount.
| Product Category | Operating Voltage | LED Density / m² | Cut Point Flex | Max Single Run | Best Application Scenario |
|---|---|---|---|---|---|
| Cuttable LED Sheet Panel | DC24V | 528 - 1,296 LEDs | Every 1 LED (Matrix) | 10 Meters Roll | Translucent Marble, Quartz, Onyx Countertops & Bar Backs |
| Dual CCT 2835 Strip | DC48V / DC24V | 120 LEDs / m | 50 mm Intervals | 15 - 20 Meters | Commercial Joinery, Under-Cabinet, Human-Centric Circadian Coves |
| Dotless FCOB Strip | DC24V | 480 - 840 Chips | 15 - 25 mm Intervals | 10 Meters | Shallow Profiles (<10mm depth), Flush Wall Slot Details |
| IP67 Outdoor Neon Flex | DC24V / DC48V | 120 - 180 LEDs | 50 mm Intervals | 10 - 30 Meters | Coastal Building Facades, Outdoor Signage, Pool Perimeter Decor |
1. The Science of 48V Long-Run Circuitry
In traditional 12V or 24V strip installations, electrical resistance over 10+ meters leads to noticeable dimming at the far end of the run due to voltage drop. Covek's engineered DC48V Architecture reduces operating current by 50% compared to 24V systems ($P = V \times I$). This permits run lengths up to 20 meters fed from a single power point without color shift or lumen loss, dramatically cutting electrician installation labor hours on NZ job sites.
2. Thermal Management & 3oz Copper Double-Sided FPC
Heat is the primary cause of LED lumen depreciation. Covek backlights utilize 3oz/4oz rolled double-sided copper Flexible Printed Circuits (FPC). This thick copper substrate acts as a passive thermal sink, quickly transferring heat away from the LED dies to prevent phosphor degradation and color drifting over its 50,000-hour rated lifespan.
Localized Application Scenarios in New Zealand
Our OEM/ODM products are designed to excel under local environmental and architectural parameters.
1. Luxury Hospitality & Eco-Lodges (Queenstown & Wanaka)
Challenge: Creating warm, high-CRI, dimmable ambiance behind natural stone surfaces without thermal buildup in enclosed timber spaces.
Solution: 2700K Warm White 610*305mm Cuttable LED Backlight Sheets paired with DALI-2 / Triac smooth dimming drivers. High CRI 95+ displays natural stone veins accurately.
2. Translucent Stone Island Bars (Auckland & Christchurch)
Challenge: Stone masons requiring edge-to-edge backlight coverage without dark borders, installed within narrow 30mm air gaps.
Solution: High-density 1296-LED 10M roll-to-roll sheets with 120° wide beam angles. Uniform diffusion ensures zero spotting through 15mm-20mm translucent onyx or quartzite slabs.
3. Outdoor Facades & Marine Signage (Wellington & Tauranga)
Challenge: Exposure to salt spray, high humidity, and intense UV radiation in coastal New Zealand regions.
Solution: IP67/IP68 silicone co-extruded RGBW LED strips and neon flex featuring UV-stabilized jackets that resist cracking, yellowing, and saltwater corrosion over years of exposure.
OEM/ODM Manufacturing Capabilities & E-E-A-T Rigor
Founded in 2011, Shenzhen Covek Lighting Co., Ltd. operates a 5,175 m² state-of-the-art facility staffed by 133 specialized engineers and technical personnel. Verified onsite by independent inspection authority TÜV Rheinland, our manufacturing plant operates strictly under the ISO 9001 Quality Management System.
Advanced SMT Lines
High-speed Yamaha SMT placement lines ensuring precision mounting of SMD2835, SMD5050, and Flip-Chip (FCOB) components onto ultra-long continuous flexible PCBs.
Integrating Sphere Binning
Every production batch undergoes strict chromaticity testing. We guarantee color consistency within a 3-Step MacAdam Ellipse across re-orders for project expansions.
100% 8-Hour Burn-In Testing
Zero-defect quality policy. 100% of finished flexible backlight sheets and strips undergo high-voltage stress testing and 8-hour continuous burn-in before export packaging.
For New Zealand importers, electrical merchants, and OEM brands, Covek provides comprehensive custom manufacturing services including:
- Custom PCB Layout & Logo Printing: Your brand logo laser-etched onto double-sided white/black FPC backing.
- Tailored Cable Harnessing: Factory-soldered IP67 quick-connect waterproof pigtails, tailored to exact site dimensions.
- Regulatory Support: Complete test reports for CE, RoHS, EMC, and UL compliance submittals to local NZ inspectors.
Frequently Asked Questions (NZ B2B Sourcing)
Essential technical and commercial answers for New Zealand wholesalers, lighting designers, and contractors.
Request Custom Wholesale Pricing & Sample Kits for New Zealand Projects
Connect directly with our senior LED application engineers. Receive customized lighting layouts, photometric IES files, and wholesale factory pricing within 12 hours.
Inquire Now