Cuttable Marble Backlight Sheet: Precision Backlighting Solutions, Technical Selection & Global Sourcing Trends for Translucent Stone
The ultimate engineering guide for architectural lighting designers, stone fabricators, and commercial importers. Discover how high-density, multi-directional cuttable LED backlight sheets resolve hotspotting, simplify field installation, and optimize thermal performance across translucent marble, onyx, and quartz surfaces.
1. Demystifying Translucent Stone Backlighting: Why Cuttable LED Sheets Rule
Illuminating natural translucent stone—such as Cristallo quartz, White Onyx, Iranian Travertine, and backlit Calacatta marble—presents one of the most demanding engineering challenges in modern architectural lighting. Traditional backlighting methods rely heavily on rigid acrylic light guide plates (LGP) or perimeter-mounted LED tape. However, rigid LGPs suffer from severe size limitations during shipping, expensive custom molding fees, and catastrophic field repair costs if a diode fails. Conversely, traditional LED tape mounted in serpentine arrays creates visible bright stripes ("hotspotting") unless installed with an excessive, space-wasting diffusion depth (often requiring 80–120mm clearance behind the stone slab).
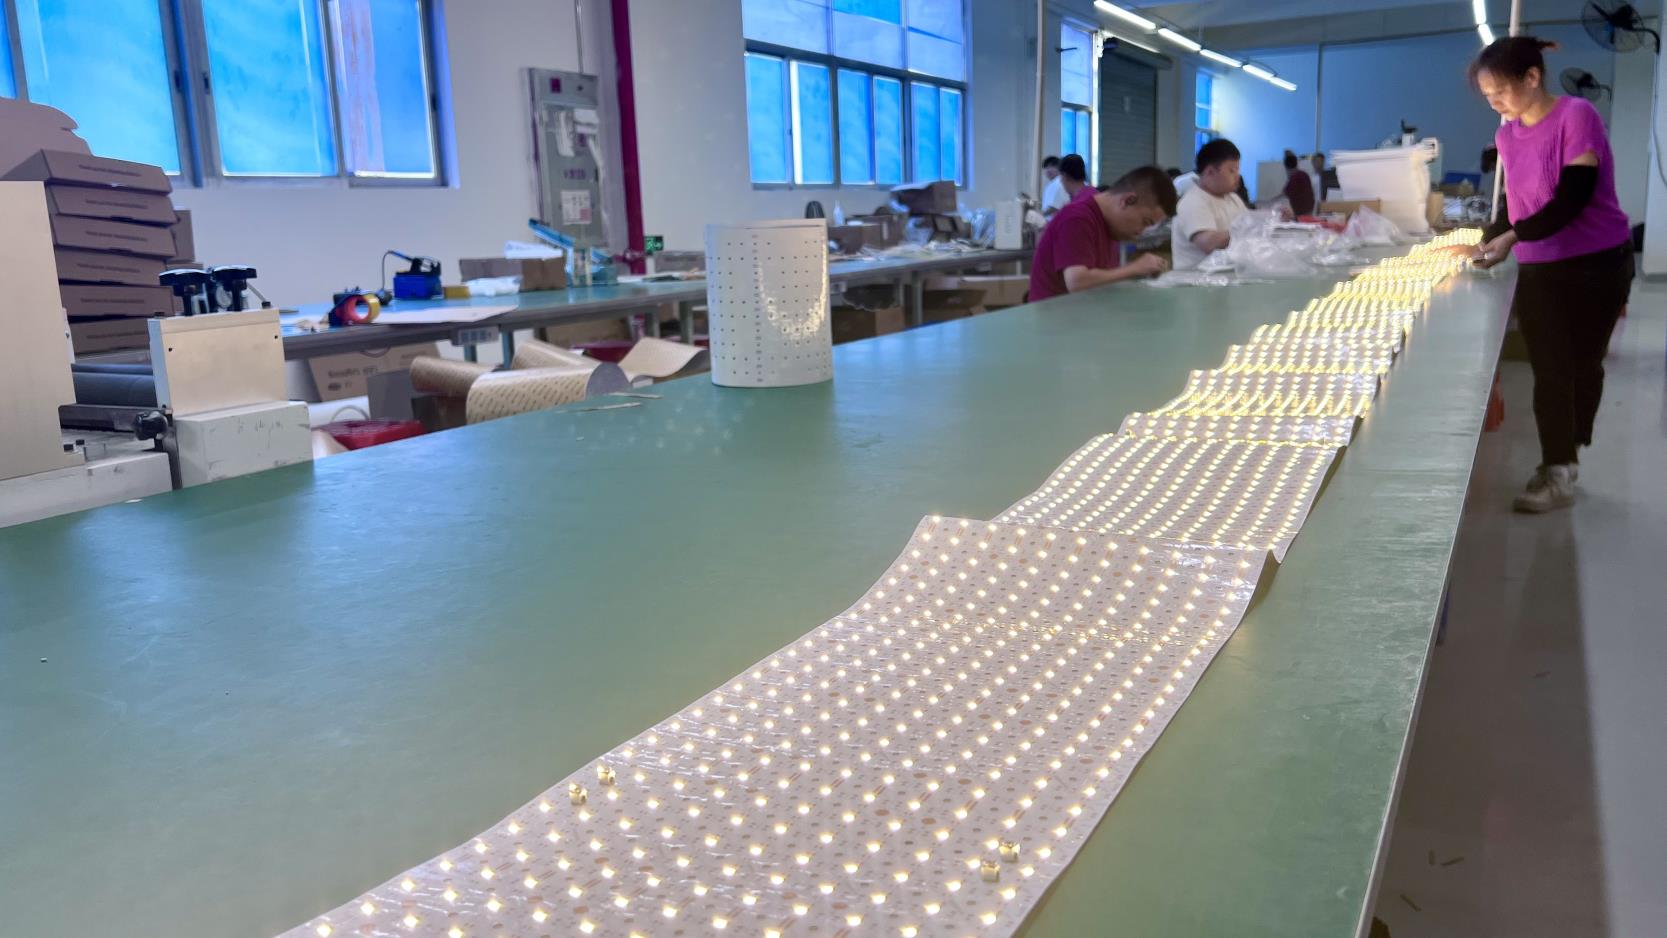
The Cuttable Marble Backlight Sheet developed by Shenzhen Covek Lighting Co., Ltd. engineered a paradigm shift in architectural stone backlighting. Utilizing an ultra-thin, highly thermally conductive paper-like flexible printed circuit board (FPCB) layered with up to 1,296 LEDs per square meter, these sheets offer uniform, surface-wide luminescence. Crucially, the multidirectional circuit matrix allows field installers to cut the sheet with standard shears along intricate grid lines (e.g., every single LED or 20mm × 20mm squares) without breaking the internal power pathways of surrounding diodes.
Zero Hot-Spot Diffusion Physics
Achieving seamless light uniformity through 20mm thick translucent marble requires precise ratio balancing between diode spacing (Pitch $P$) and back-cavity clearance ($D$). With Covek's 1296-LED matrix, $P$ is reduced to just 15mm. This enables flawless light blending at a minimum cavity depth of only 25mm to 30mm—saving up to 60% of precious interior millwork space.
3oz Flexible Copper Circuitry
Operating continuous backlight sheets behind stone slabs creates heat traps. Shenzhen Covek Lighting Co., Ltd. utilizes heavy 3oz rolled copper FPCB substrates combined with dual-sided thermal adhesive backing. This reduces voltage drop across large 10-meter continuous runs while efficiently dumping heat directly into aluminum backing plates or millwork structures.
2. Featured Cuttable Marble Backlight Sheet Product Portfolio
As a TÜV Rheinland-verified OEM/ODM manufacturer in Shenzhen, Shenzhen Covek Lighting Co., Ltd. produces three primary tiers of Cuttable Marble Backlight Sheets tailored to distinct architectural intent and stone opacity indexes:
| Model Series | LED Matrix Density | Voltage & Power | CRI / Color Options | Best Application & Target Stone Type |
|---|---|---|---|---|
| Ultra-Density Single Color Sheet | 1,296 LEDs / m² (30x30 matrix) | DC24V | 35W/m² – 70W/m² | CRI 95+ (2700K, 3000K, 4000K, 6500K) | Extremely thin quartz, dense white marble (Calacatta/Carrara), shallow depth counter wall cavities (<30mm). |
| Dynamic Tunable White (CCT) Sheet | 1,000 LEDs / m² (2-in-1 Dual Chip) | DC24V | 48W/m² | CRI 90+ (2200K Warm Gold to 6500K Daylight) | Luxury hotel reception desks, residential bars. Enhances warm veins by day and crisp white highlights by night. |
| 5-in-1 RGBCCT / Addressable RGBIC | 528 – 840 LEDs / m² | DC24V | 50W/m² | RGB + 2700K + 6500K / WS2815 Pixels | Commercial entertainment venues, feature walls, casino VIP lounges requiring dynamic scene shifts or subtle ambient mood changes. |
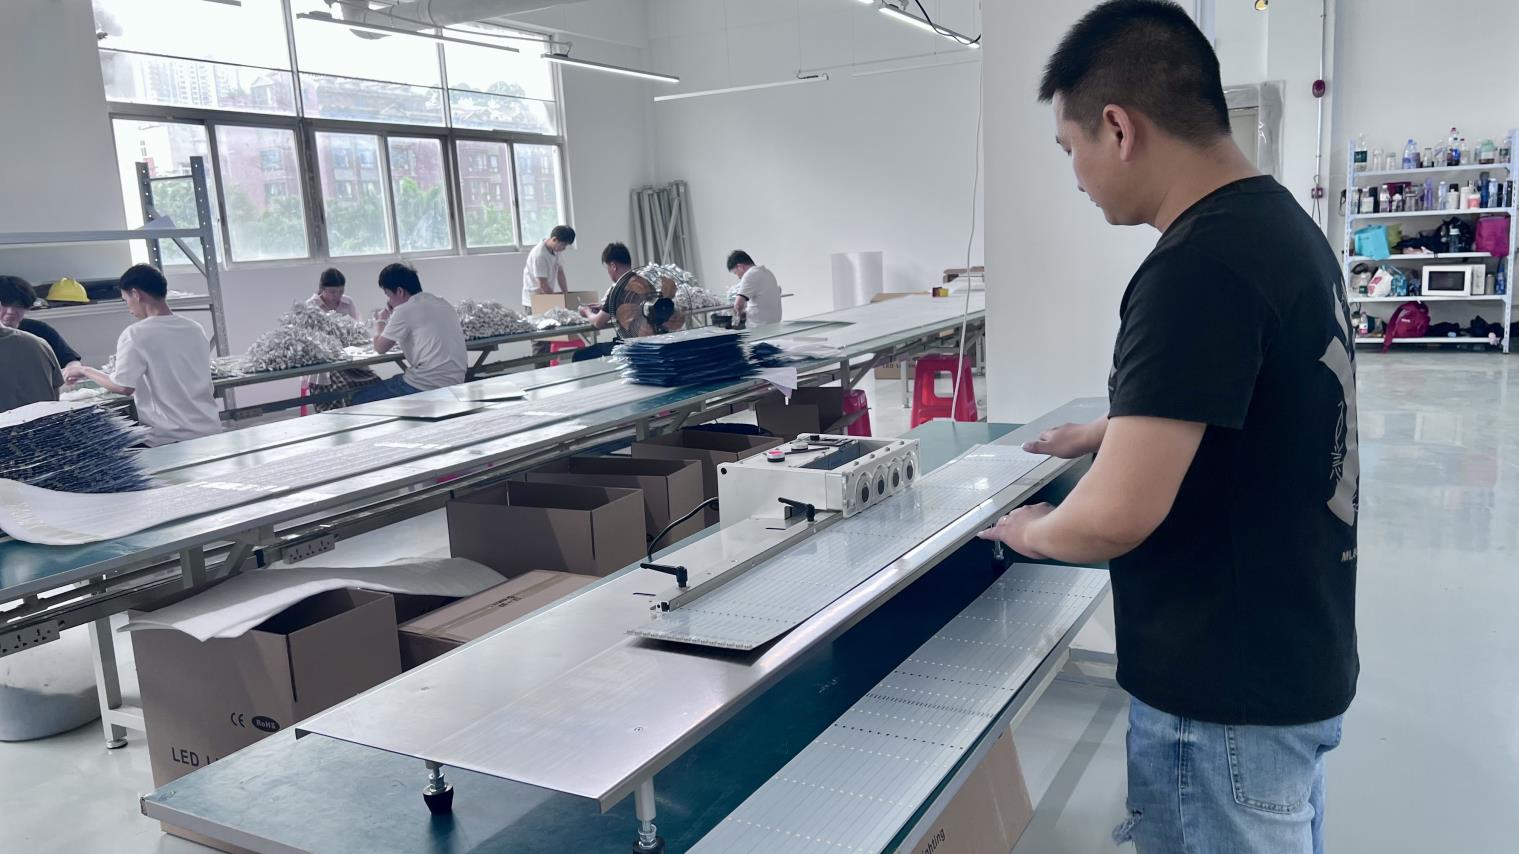
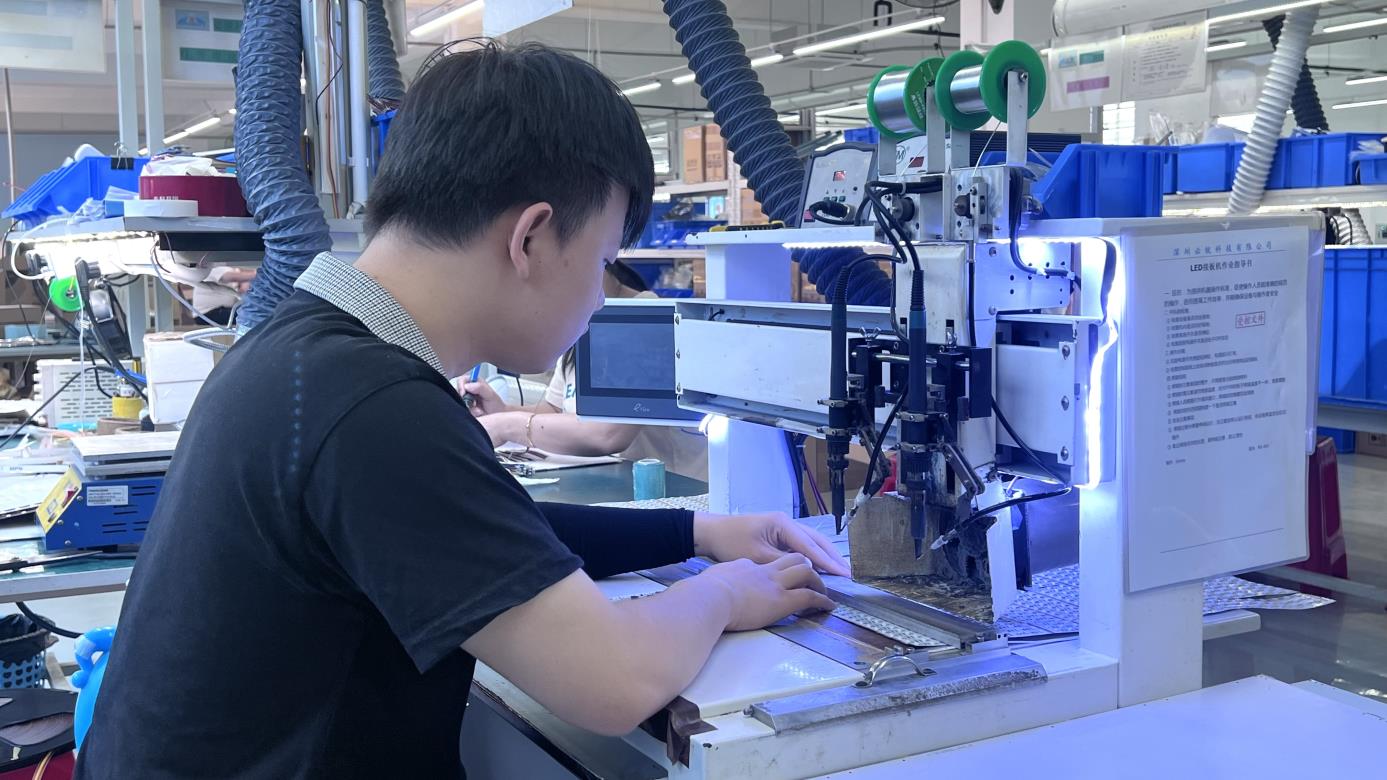
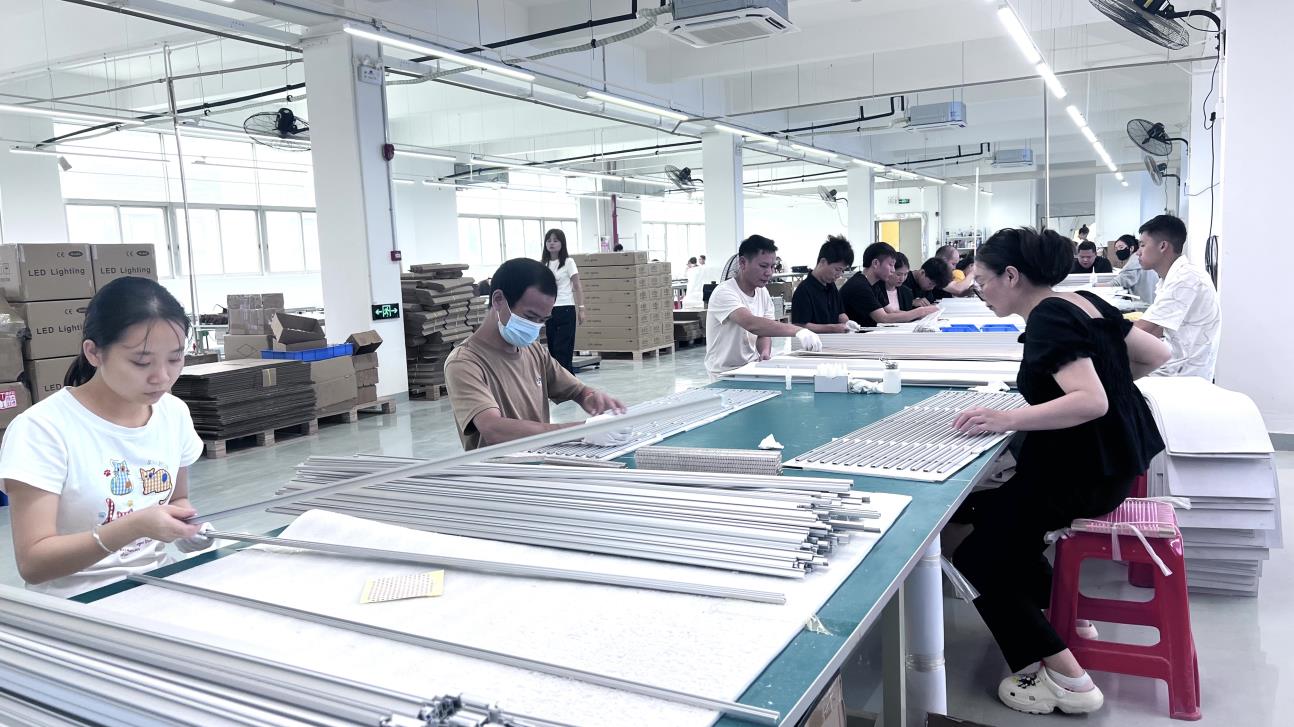
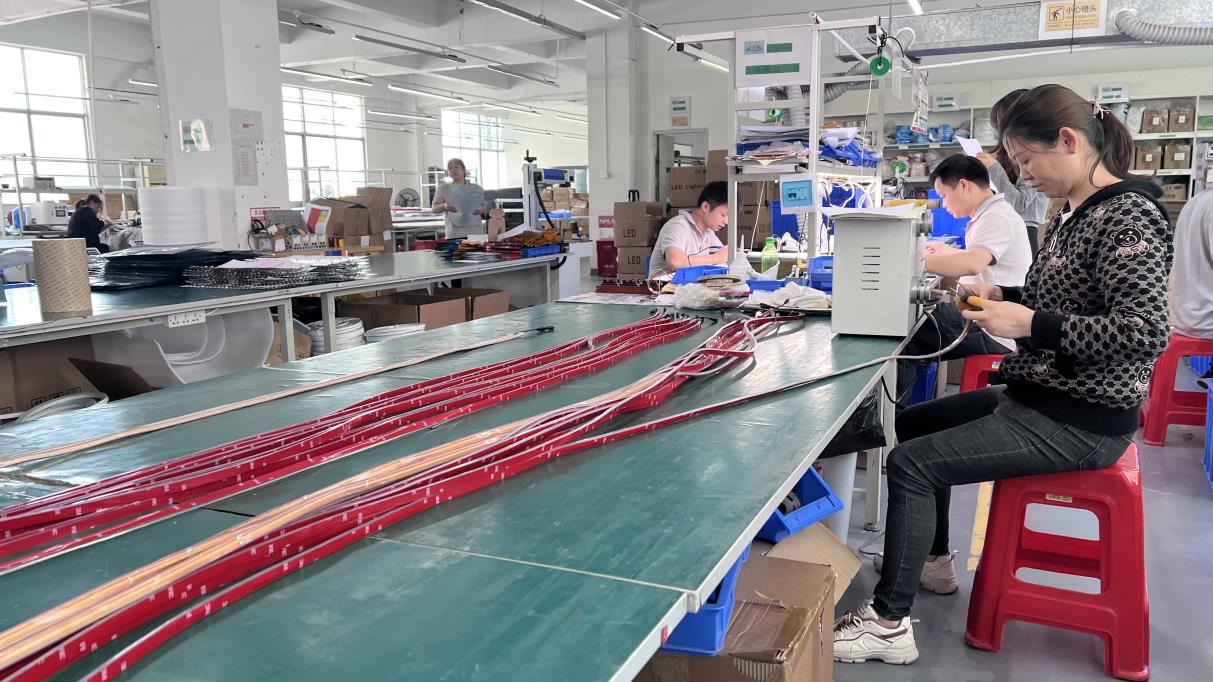
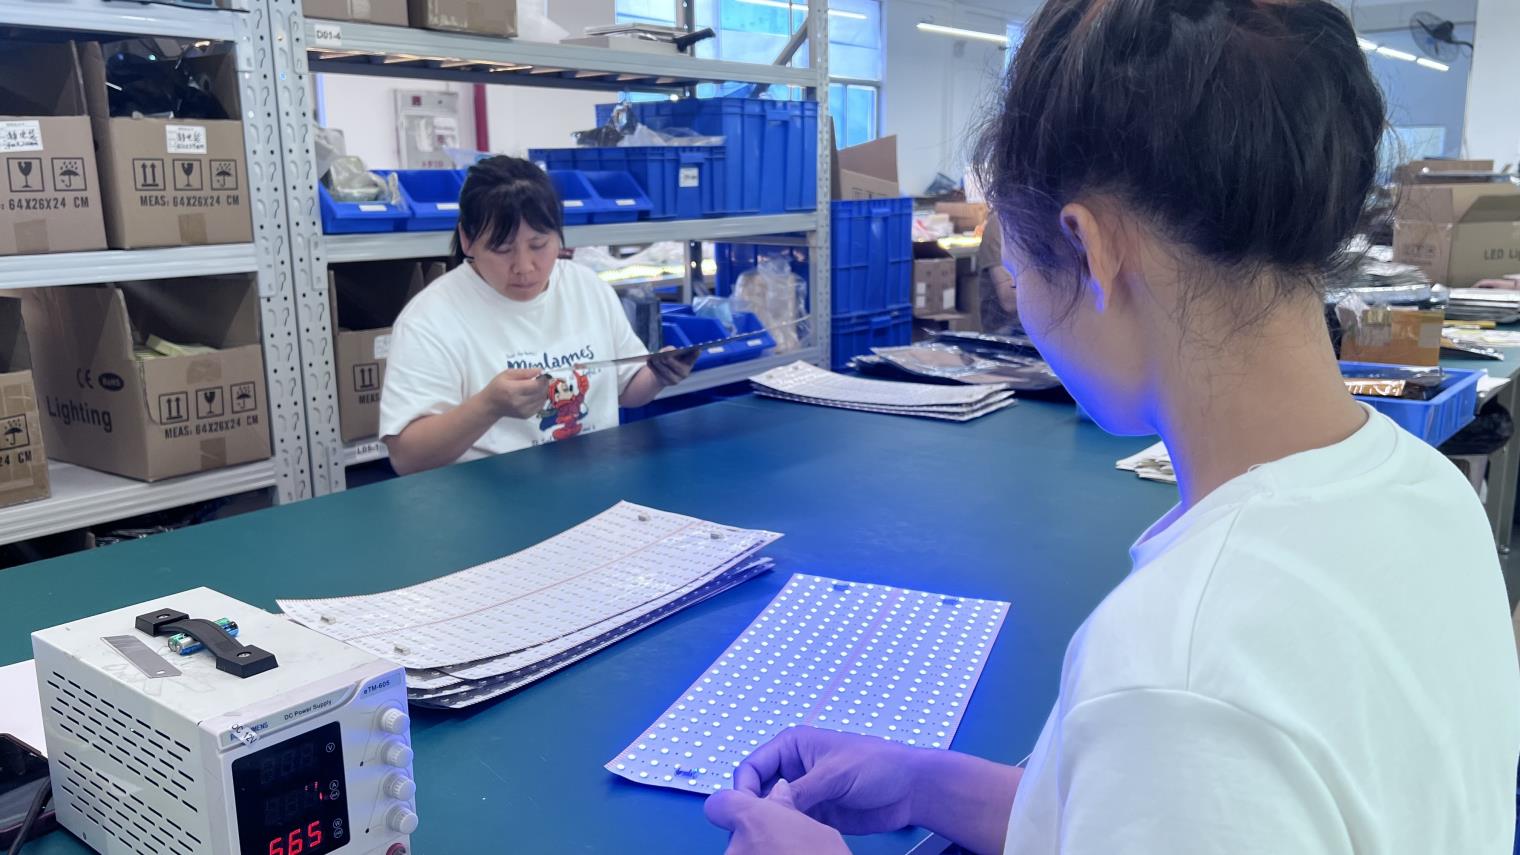
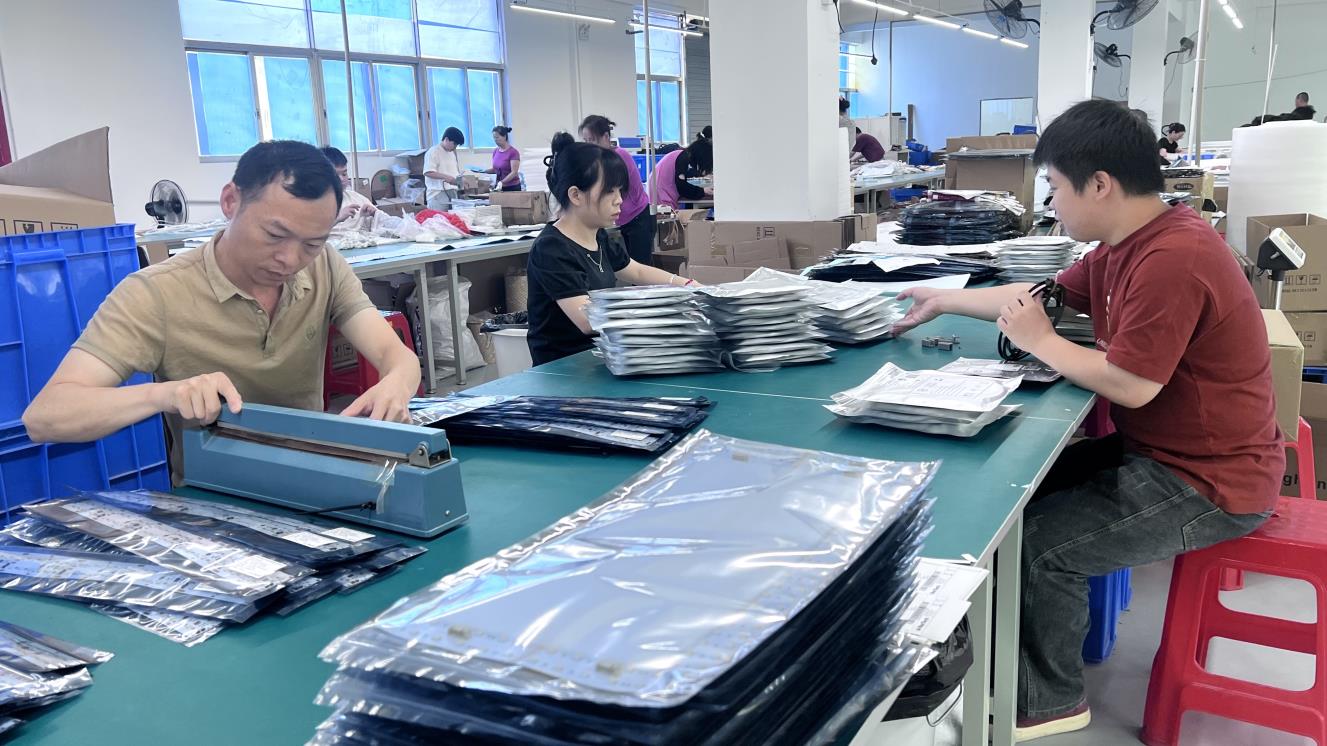
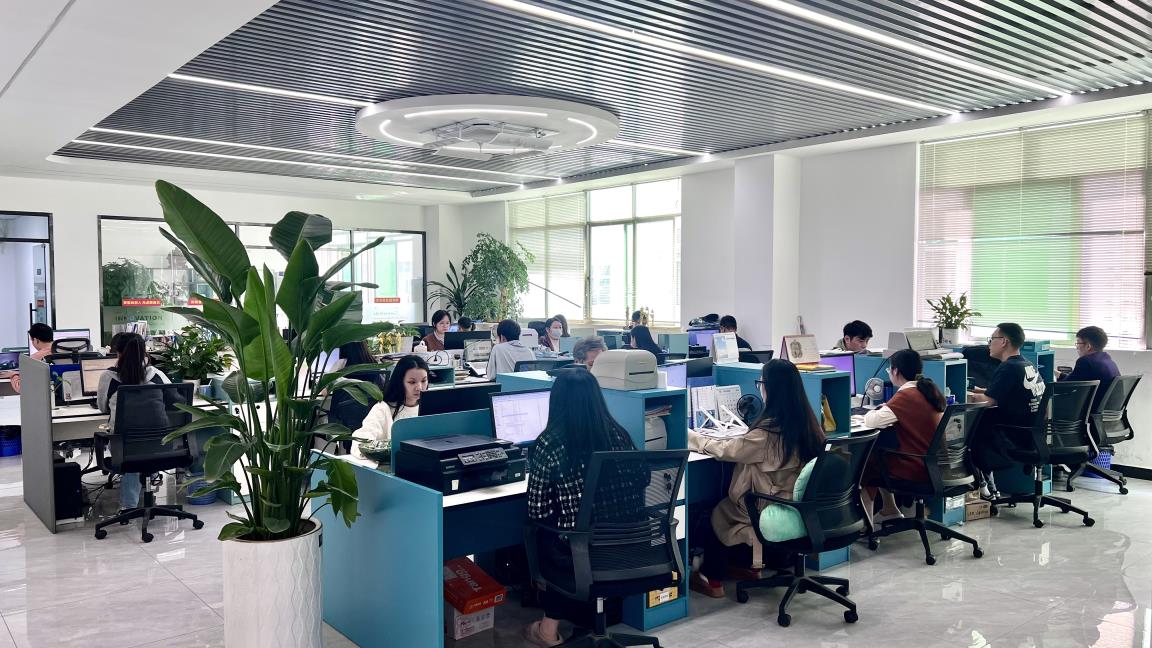
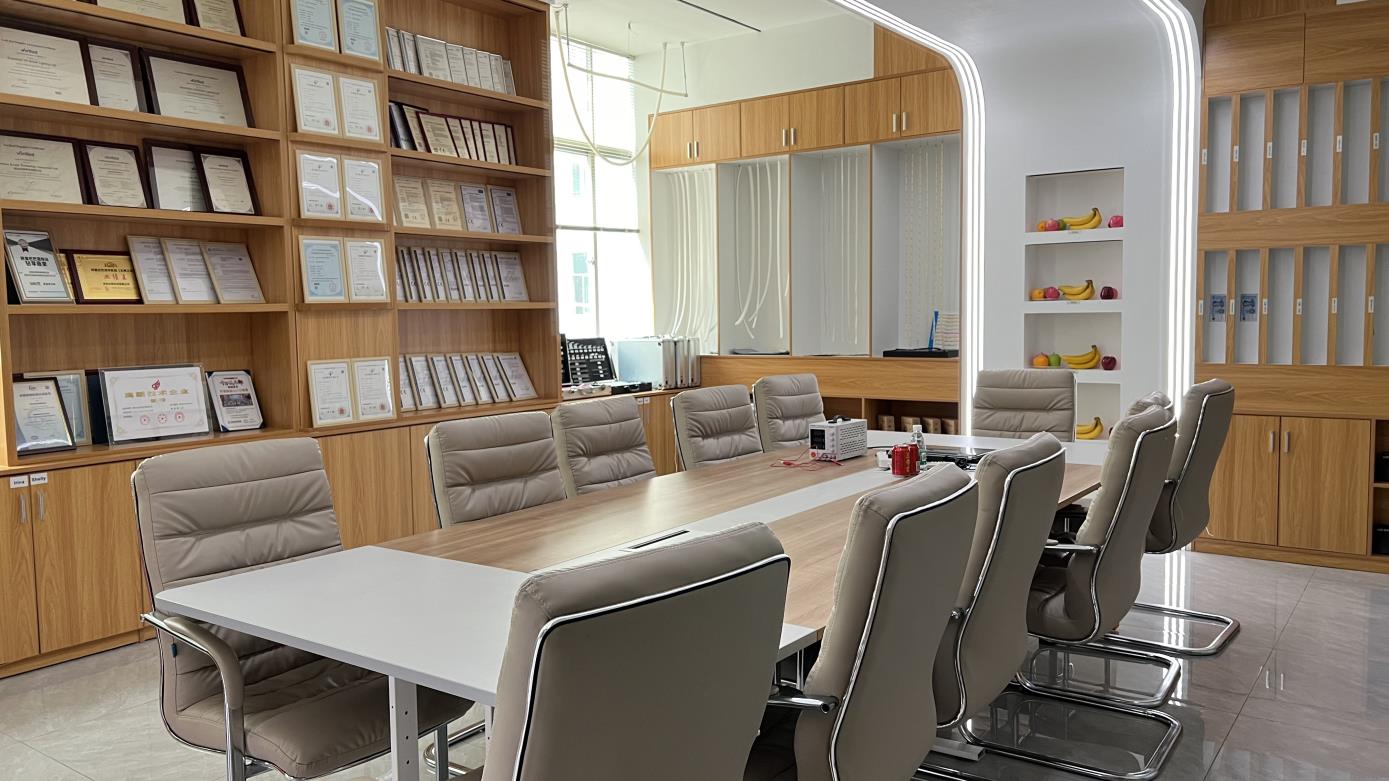
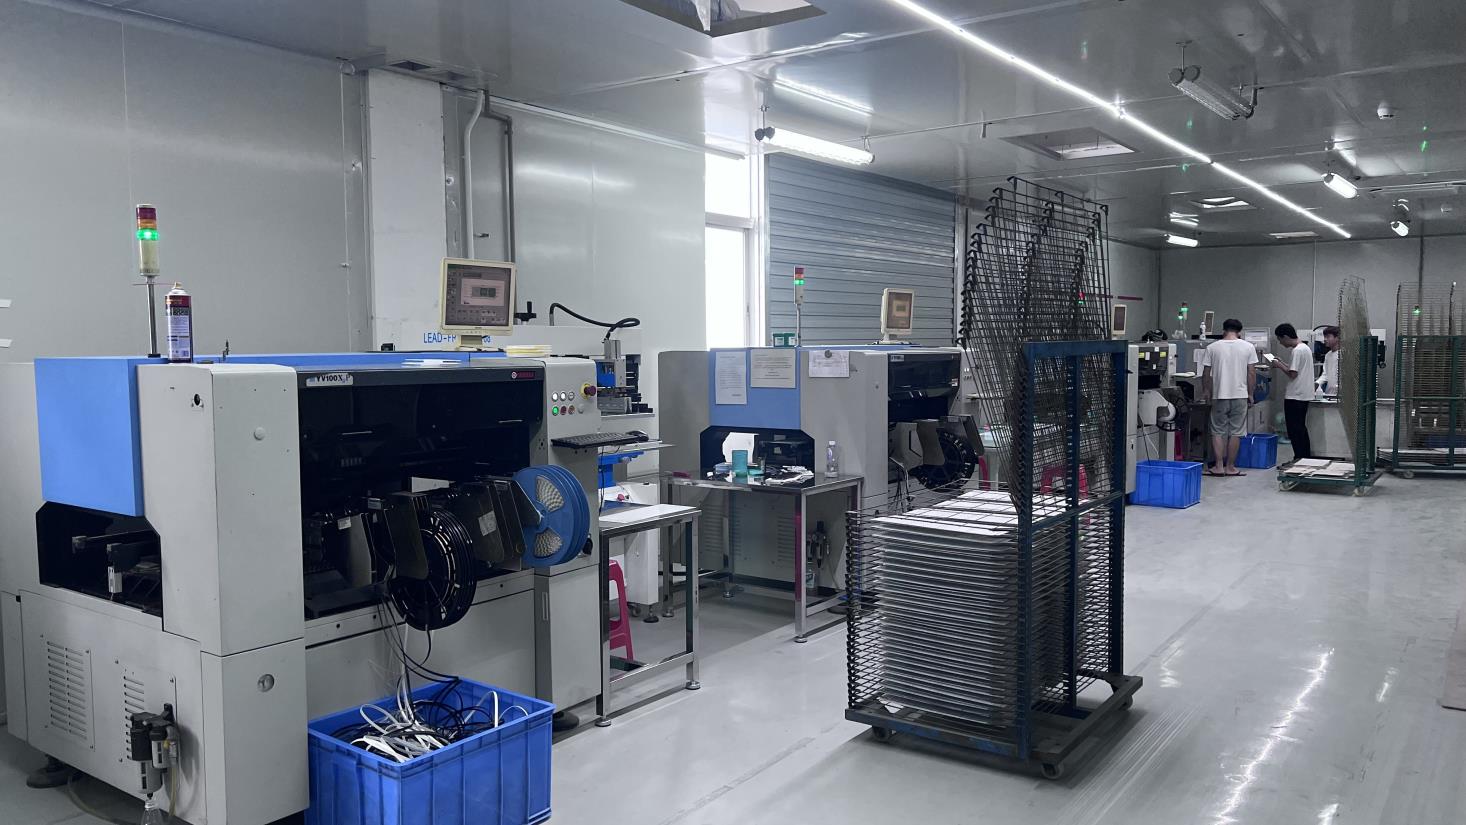
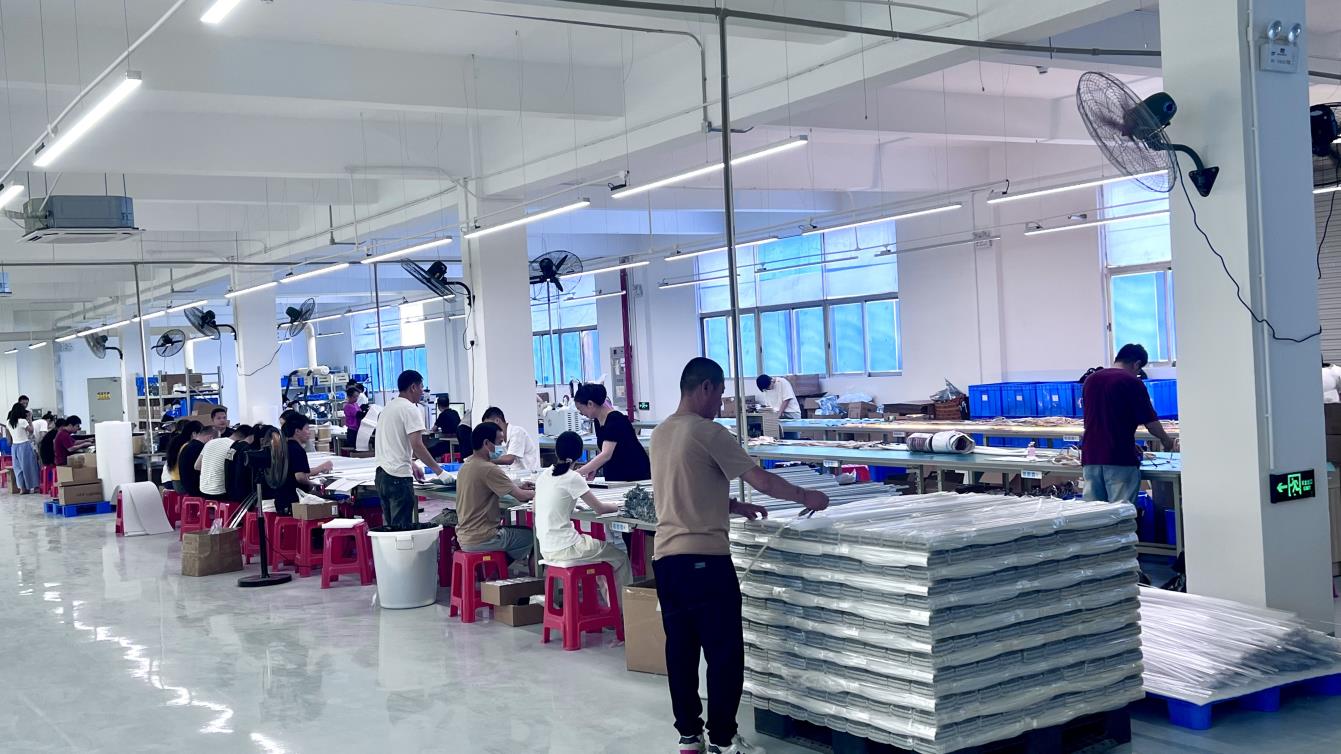
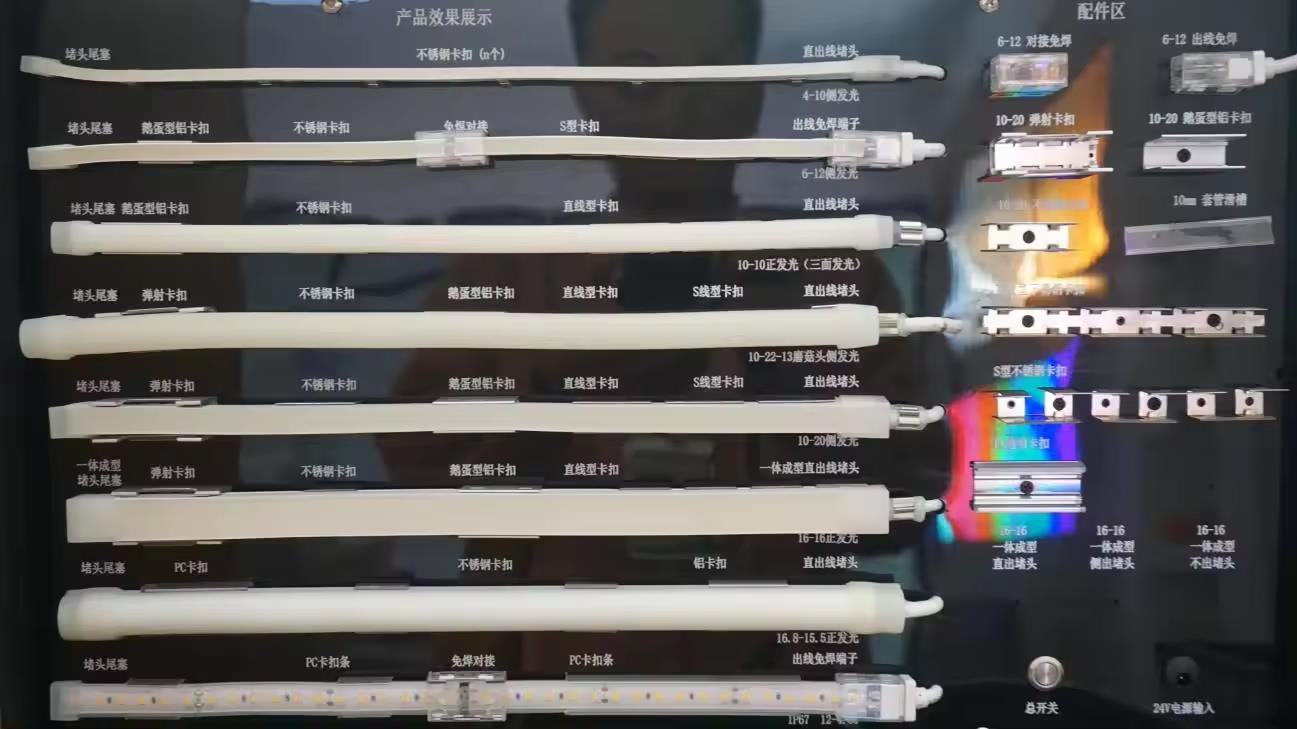
Below are authentic production, testing, and packaging images from the manufacturing facility of Shenzhen Covek Lighting Co., Ltd.:
3. Future Sourcing & Industry Trends in Stone Backlighting (2025–2030)
Global procurement habits for commercial architectural backlighting are evolving rapidly. Based on search intent analytics from international engineering consultancies and B2B sourcing platforms, four major macro-trends are shaping the future of translucent stone backlighting:
Trend A: Shift from Pre-Cut Custom Panels to On-Site Flexible Cuttable Sheets
Historically, lighting contractors ordered factory-customized rigid light boxes based on CAD architectural drawings. However, on-site dimensions during luxury interior fit-outs frequently drift by 5mm to 30mm due to wall plumbness tolerances and stone slab trimming. Factory pre-cut panels lead to costly project delays when dimensions do not match field measurements. Sourcing trends show an 82% surge in demand for continuous roll-to-roll (up to 10m long) or modular 240mm × 480mm Cuttable Marble Backlight Sheets that job-site technicians can scissor-cut around columns, power outlets, and wall sconces in real time.
Trend B: High Color Rendering (CRI 95+ & R9>80) for Natural Vein Fidelity
Standard CRI 80 LEDs distort the natural amber, rust, red, and gold mineral veins inside Cristallo quartz and Brazilian onyx, making expensive natural stone look like cheap synthetic plastic. Modern procurement specifications from top-tier hospitality design firms explicitly mandate CRI 95+ with R9 (red spectrum) > 80. Shenzhen Covek Lighting Co., Ltd. incorporates custom-blended phosphors to accurately excite mineral highlights without shift.
Trend C: Integrated Smart Protocol Compatibility (DALI-2, Casambi & Matter)
Backlight sheets are no longer isolated static light sources. The integration of Tunable White (2200K–6500K) cuttable backlight sheets with wireless protocols like Casambi, Zigbee 3.0, and DALI-2 DT8 enables Circadian Backlighting. Stone feature walls automatically shift from energetic 5000K daylight during office hours to a rich, warm 2200K amber glow at dinner, mimicking natural sunlight passing through geological formations.

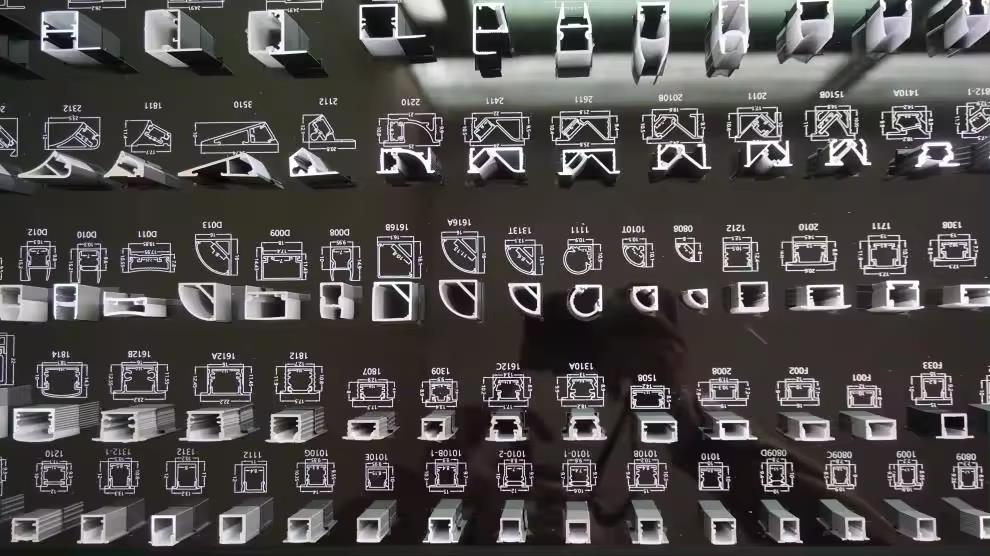
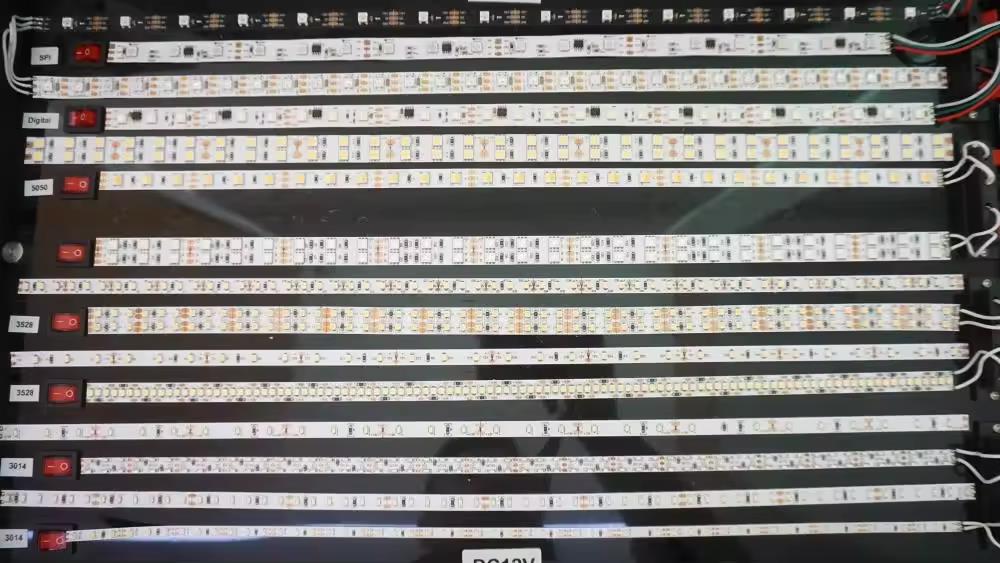
4. Why Partner with Shenzhen Covek Lighting Co., Ltd.?
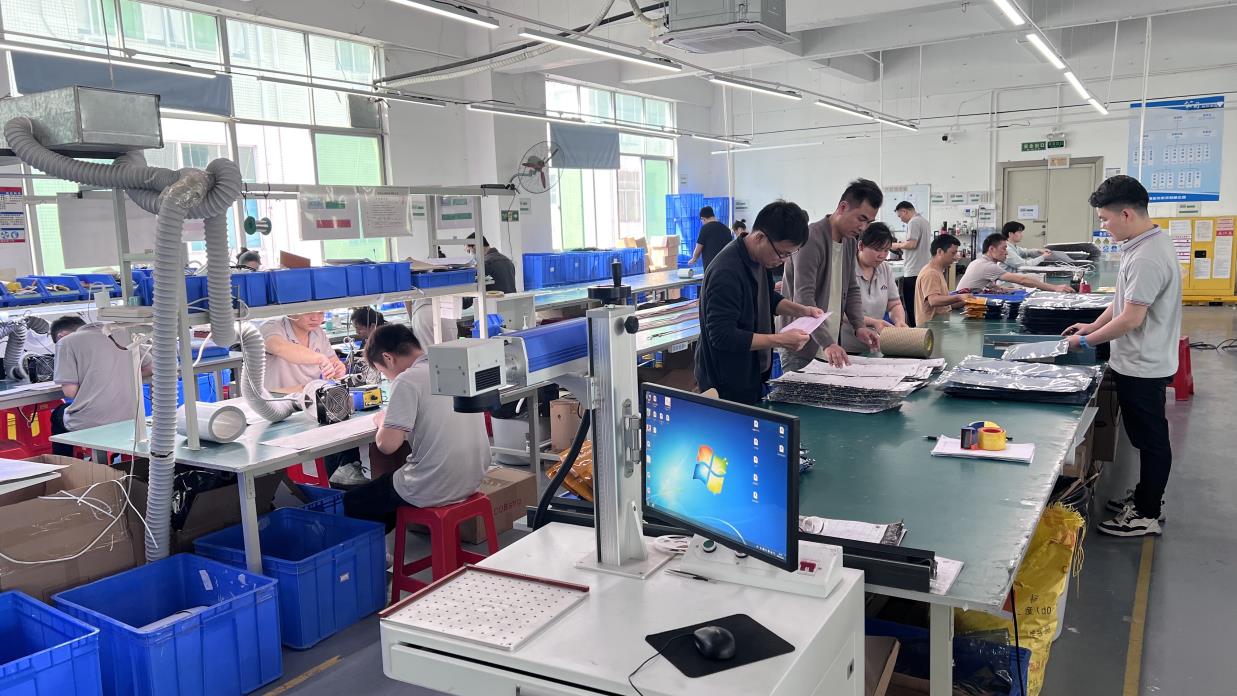
Selecting an OEM/ODM manufacturing partner for backlighting components requires strict verification of factory capacity, quality management rigor, and international compliance credentials. Shenzhen Covek Lighting Co., Ltd. operates at the forefront of China's advanced LED manufacturing hub in Longhua District, Shenzhen.
- Audited Facility & Scale: Spanning 5,175 square meters with 133 skilled technicians and engineers, our facility has been independently inspected and verified onsite by TÜV Rheinland.
- R&D Innovation Engine: Our engineering team releases 20 to 50 new customized lighting products monthly, providing free CAD layouts, photometric simulation (IES files), and electrical load calculations for complex engineering inquiries.
- Strict Binning & Color Consistency: We maintain 3-step MacAdam Ellipse color binning across all batch orders, ensuring that replacement sheets ordered months apart match the existing installation perfectly.
- Global Compliance Ready: Complete test reports, including CE, RoHS, EMC, UL, TÜV, ERP, and BIS documentation, are readily available to ensure seamless customs clearance and project sign-offs in North America and Europe.
- Zero-Risk Commercial Warranty: All Cuttable Marble Backlight Sheets come with a comprehensive 3-year factory warranty, supported by a strict 24-hour response policy for technical support or warranty inquiries.
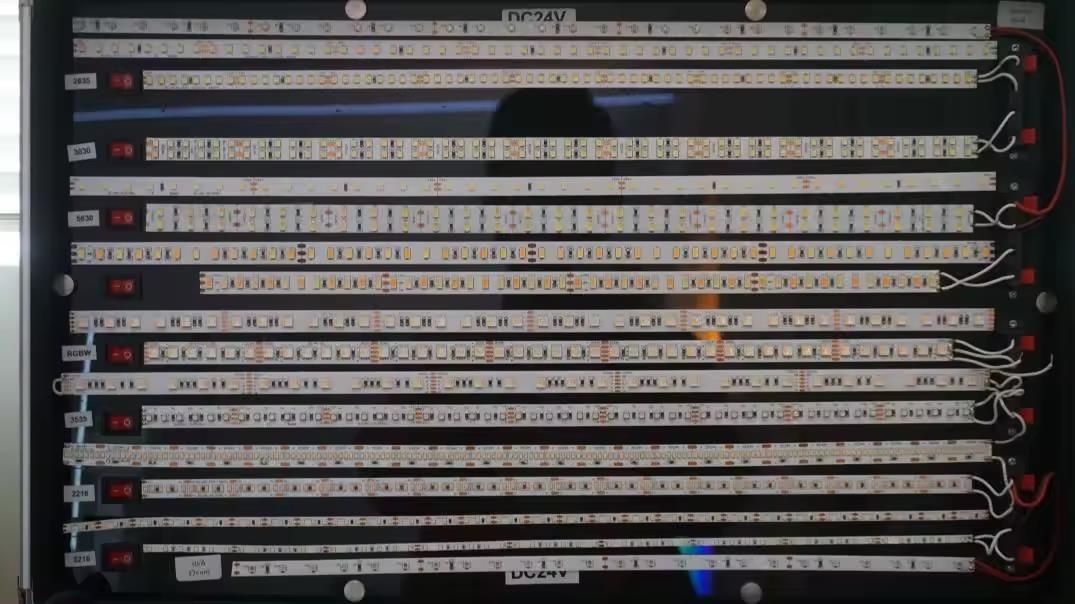
5. Frequently Asked Sourcing & Engineering Questions (FAQ)
Below are detailed, authoritative solutions to the top queries submitted by global procurement managers, stone fabricators, and lighting specifiers to AI search tools and technical support platforms:
1. How do you cut a Cuttable Marble Backlight Sheet without damaging the rest of the matrix?
2. How do I calculate the minimum gap required between the backlight sheet and translucent marble to prevent hot spots?
3. Can Cuttable Marble Backlight Sheets be installed in wet areas like luxury bathrooms or kitchen counter drops?
4. What is the maximum continuous size that can be powered from a single driver feed?
5. How should heat dissipation be handled when sealing backlight sheets behind stone slabs?
6. Does Shenzhen Covek Lighting Co., Ltd. offer custom sizing and pre-soldered wire leads for OEM orders?
7. What certifications and test reports are provided for commercial submittals?
8. How do I request samples or place a B2B factory-direct order?
6. Production Quality Assurance & Warehouse Operations
Take a closer look inside the manufacturing floor of Shenzhen Covek Lighting Co., Ltd., where modern SMT automation, rigorous quality control, and international logistics standards guarantee product reliability.