Precision-Engineered LED Backlight Sheet Portfolio
Explore our TÜV-verified cuttable LED light sheets, ultra-long matrix rolls, and high-CRI flexible strips customized for translucent marble, onyx, and quartzite illumination in Heredia.

Architectural Backlighting Dynamics in Heredia & The Central Valley
The province of Heredia, Costa Rica—known as the commercial and industrial heartland of the Greater Metropolitan Area (GAM)—is experiencing an architectural renaissance. From the high-tech office parks in Global Park, Ultrapark, and America Free Zone (AFZ) to luxury residential compounds in San Antonio de Belén, Barva, and San Rafael, contemporary interior design demands a fusion of organic stone aesthetics and cutting-edge solid-state illumination. Translucent stone surfaces—including imported Italian Cristallo Quartzite, Iranian White Onyx, Brazilian Patagonia Granite, and translucent alabaster—have become signatures of prestige in executive lobbies, luxury hotel reception desks, and high-end residential kitchen islands.
However, illuminating natural stone surfaces presents complex photometrical and thermal challenges. Unlike standard sign boxes or plastic diffusers, natural marble slabs vary dramatically in crystalline structure, mineral vein density, and light transmittance (ranging from 5% to 45%). Achieving seamless, hot-spot-free surface luminance requires a high-density LED matrix panel supplier capable of engineering custom power densities, precise color rendering indices (CRI > 95), and robust thermal management systems suited for Central America's tropical ambient conditions.
Key Technical Demands for Stone Backlighting in Tropical Climates
Exporting backlight panels to Heredia requires accounting for localized microclimates and regional structural specs. Electrical contractors and stone fabricators in Heredia encounter specific site variables:
- Ambient Humidity & Mold Resistance: Heredia’s mountainous microclimate experiences humidity levels exceeding 85%. Standard FPC (Flexible Printed Circuit) backing without conformal coating or IP-rated encapsulation degrades rapidly. Our backlight panels feature hydrophobic silicone coatings and anti-corrosive copper FPCs.
- Thermal Convection under Stone Slabs: Translucent quartz and marble are natural thermal insulators. Heat generated by low-grade LEDs gets trapped within shallow wall cavities (often 30mm–50mm depth), degrading LED phosphors and leading to rapid color shift (macadam ellipse divergence). Our flexible backlight sheets utilize 3oz heavy-copper FPC substrates that dissipate heat laterally across the entire surface area.
- Grid Voltage Compatibility & Dimming Systems: Costa Rica operates on a 120V / 60Hz single-phase or 208V 3-phase grid. Backlighting installations require premium power drivers capable of taking 120V-277V AC input and stepping down to smooth, flicker-free DC 24V or DC 48V outputs, fully integrated with 0-10V, DALI-2, or Phase-cut dimming protocols favored by Costa Rican lighting integrators.
Cuttable Matrix Topology
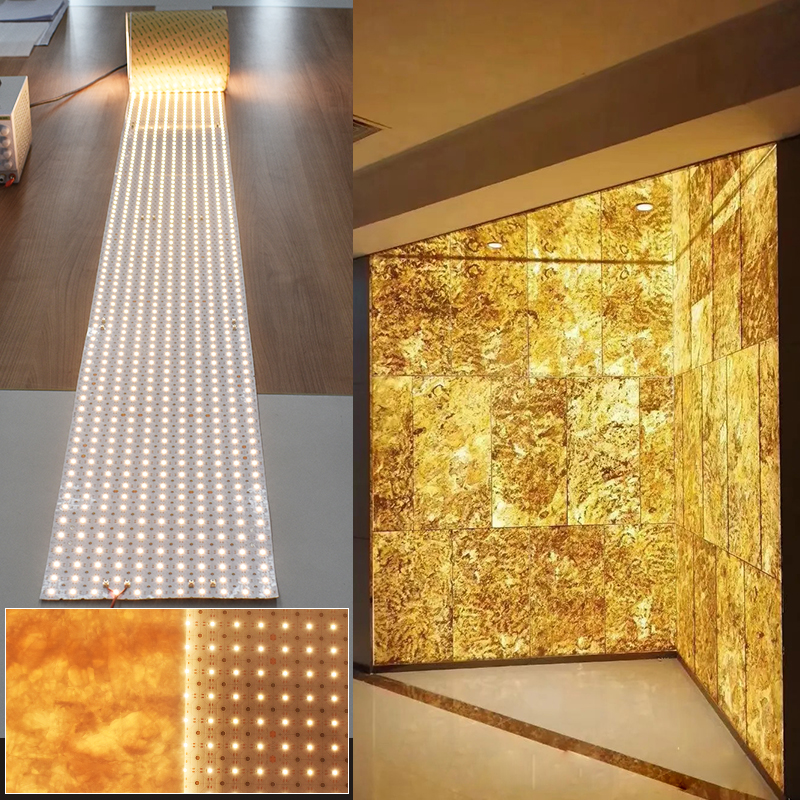
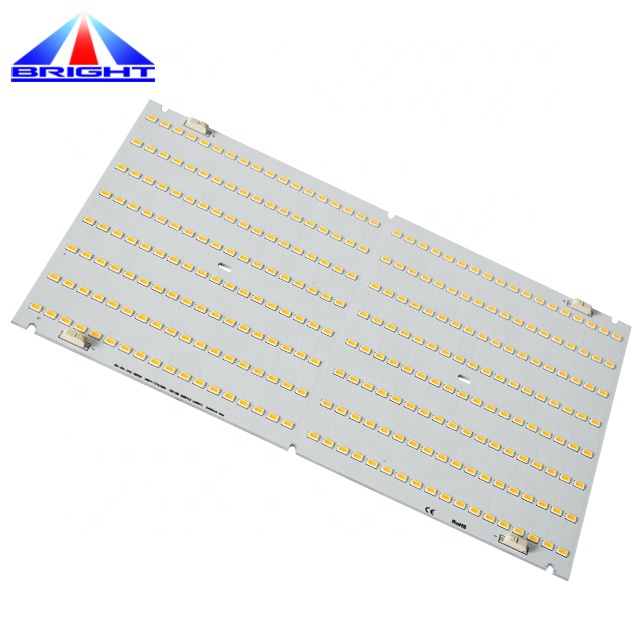
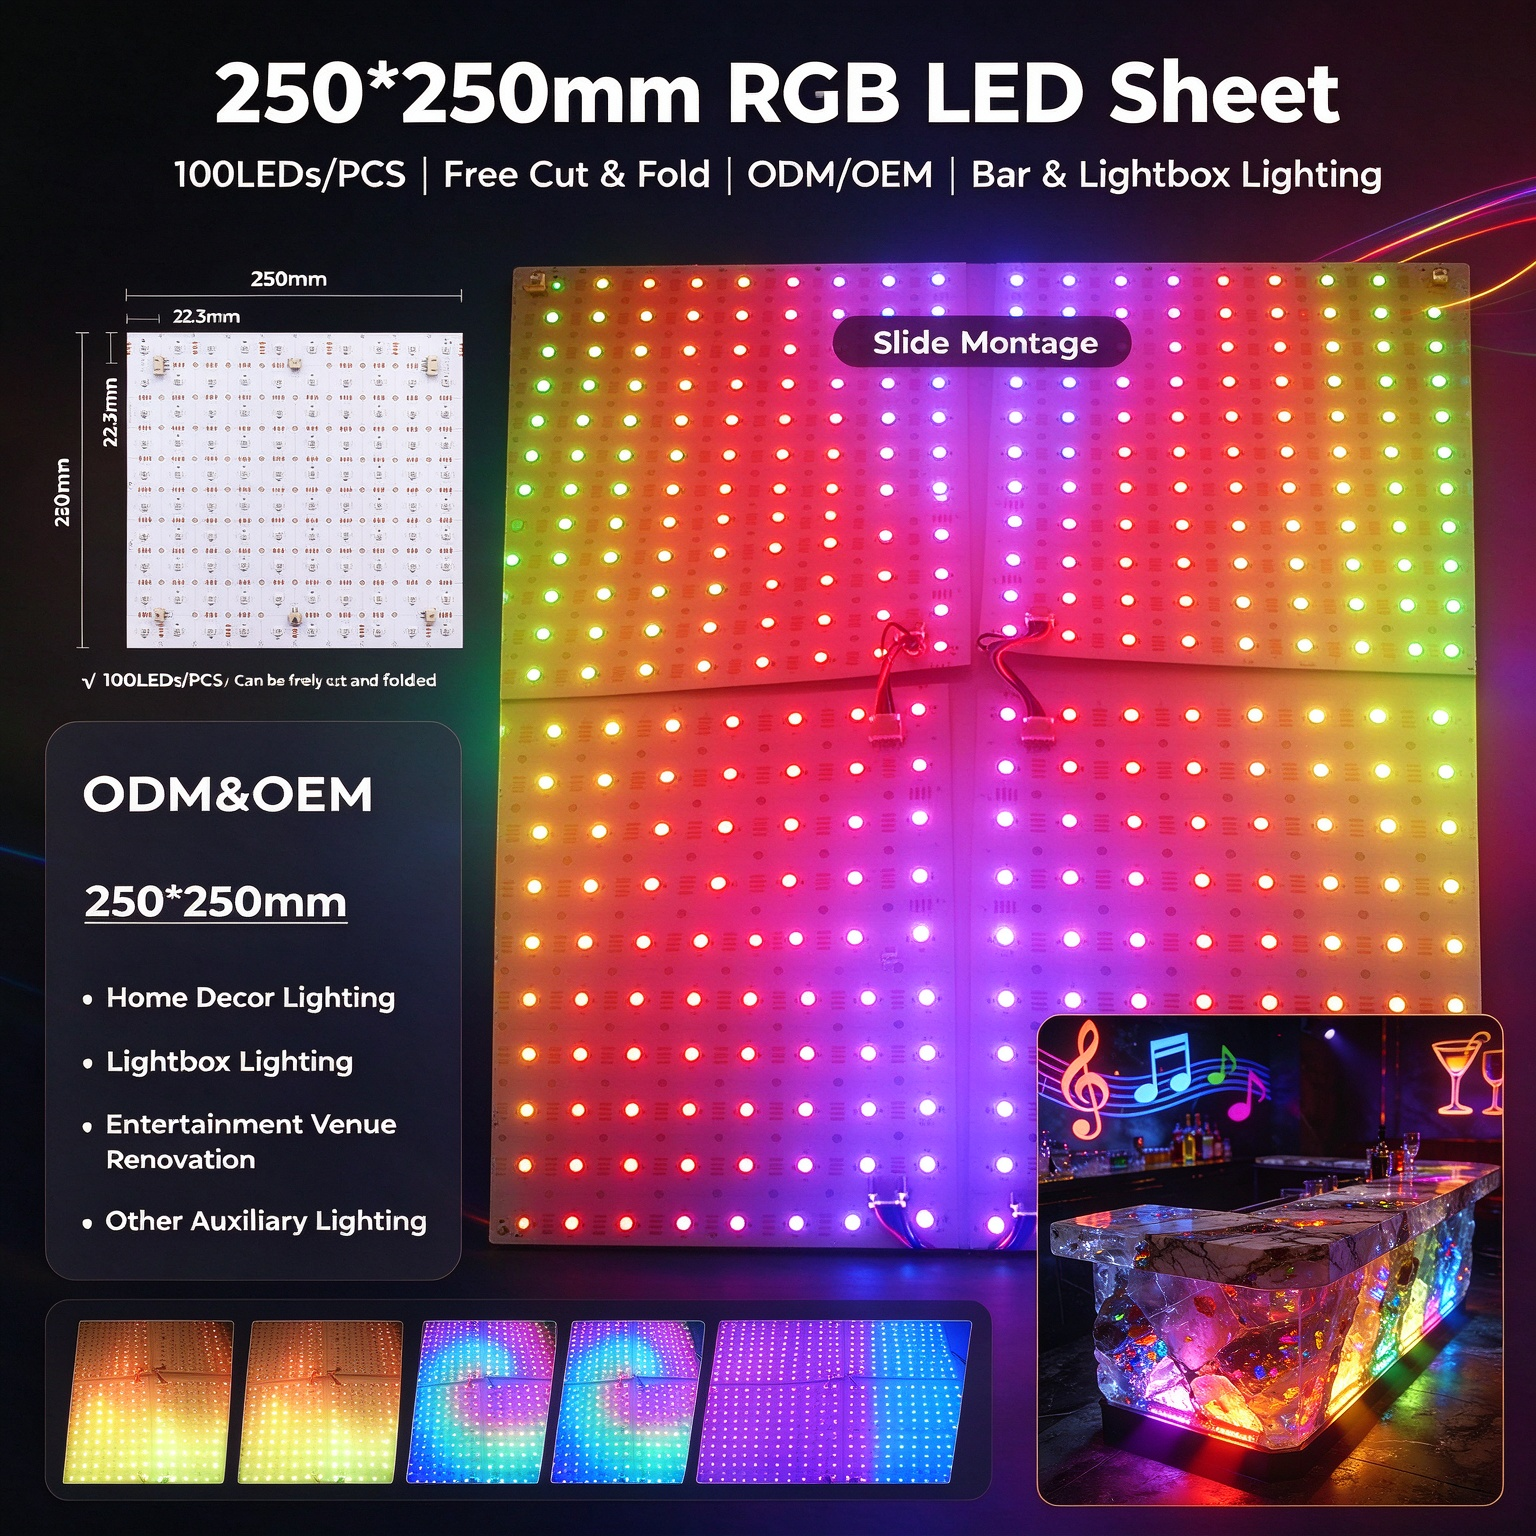
Grid-array LED sheets feature modular cutting points every single LED or 20mm grid, allowing on-site shaping around curved marble edges, sink cutouts, and structural columns without soldering extra wires.
Sunlight-Grade Spectrum (CRI > 95)
Equipped with high-R9 and high-R12 phosphors, our light engines render the deep rusts, gold veins, and subtle translucent blues of natural Costa Rican marble projects without greenish spectrum distortions.
100% Dotless Diffusion
Engineered pitch ratios (LED-to-LED distance vs. distance-to-stone depth) guarantee uniform field illumination even with shallow air gaps as low as 15mm, eliminating visible grid shadowing.
The Physics of Translucent Stone Illumination: Calculating Distance-to-Pitch Ratios
One of the most frequent structural errors committed by interior contractors in the Heredia market is miscalculating the ratio between LED diode spacing (pitch $P$) and the diffusion cavity depth ($D$). When backlighting translucent marble or engineered resin, if the cavity depth is too shallow relative to diode spacing, harsh optical bright spots (known as the "ladder effect") ruin the stone's luxury aesthetic.
Our engineering team at Shenzhen Covek Lighting utilizes the golden optical ratio for stone backlighting:
For instance, our ultra-high-density 1296-LED/m² roll-to-roll LED light sheet features a diode pitch of just 12.5mm. Applying our optical formula, the minimum required air gap behind a 20mm slab of Costa Rican translucent quartz is merely 10.6mm. This ultra-thin profile allows architects in Belén and Heredia to maximize interior floor space in boutique hotel lobbies and executive bars without requiring bulky 100mm build-outs.
Tunable White CCT Dynamic Spectrum Tuning (2700K to 6500K)
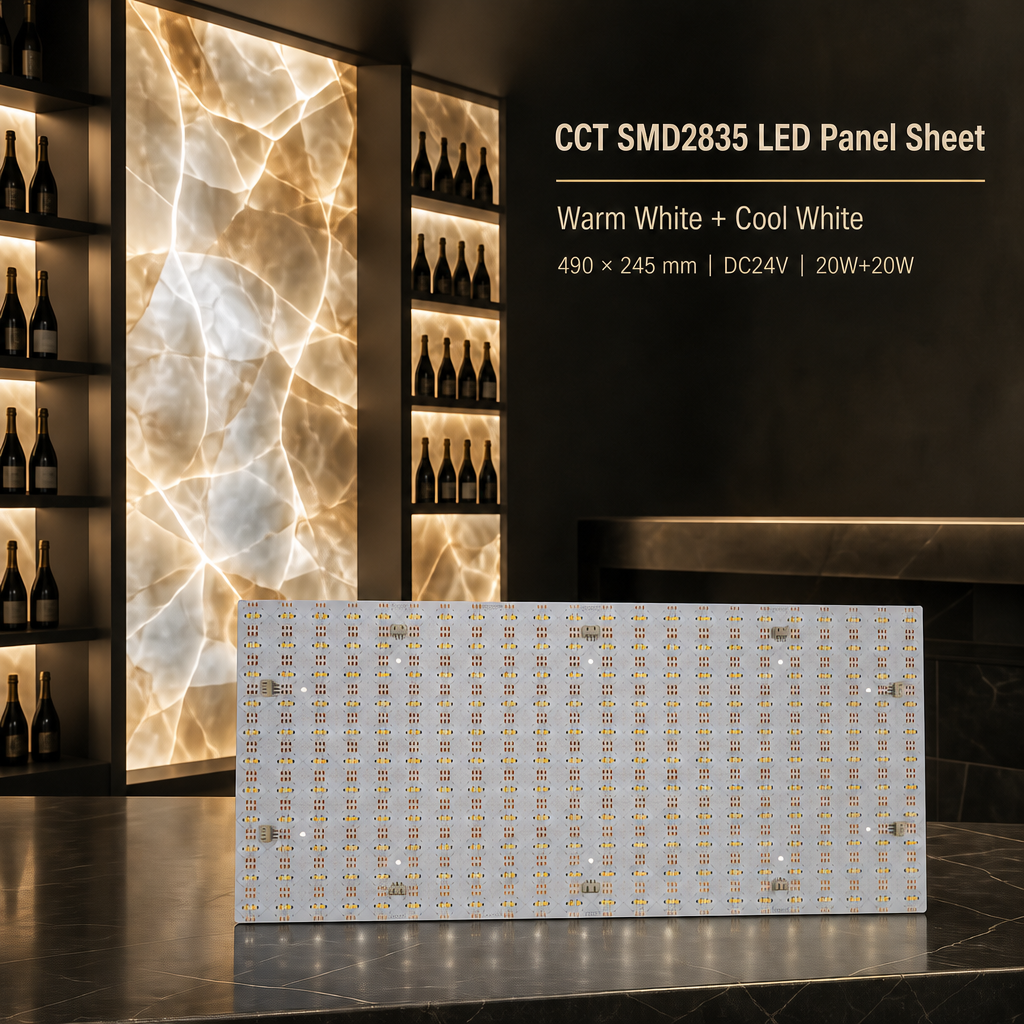
Natural stone reacts dynamically to different color temperatures. Warm vein structures in Amber Onyx radiate luxury when lit by 2700K ultra-warm white, whereas cold white 6500K accents emphasize the crisp, ice-like crystalline structure of White Cristallo Quartzite. Our DC24V Tunable White CCT Light Sheets incorporate dual-chip SMD2835 diodes with independent channel dimming, allowing venue managers in Heredia to shift ambiance automatically—transitioning from bright daylight (5000K) for daytime corporate meetings to romantic warm amber (2700K) for evening cocktail hours.
Localized Application Scenarios Across Heredia Projects
From corporate headquarters in free trade zones to luxury eco-resorts, explore how our backlight panel solutions transform Heredia’s architectural landscape.
Corporate Lobbies & Free Zone HQ (AFZ & Global Park)
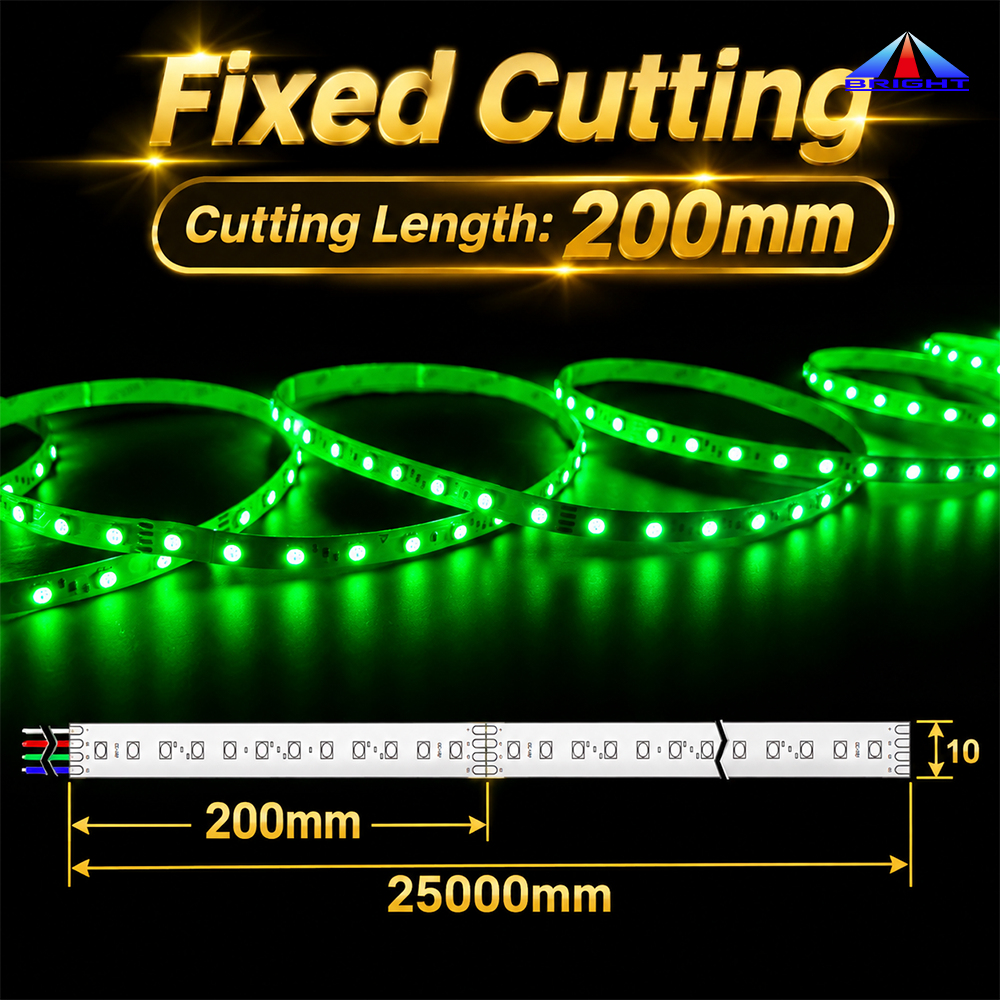
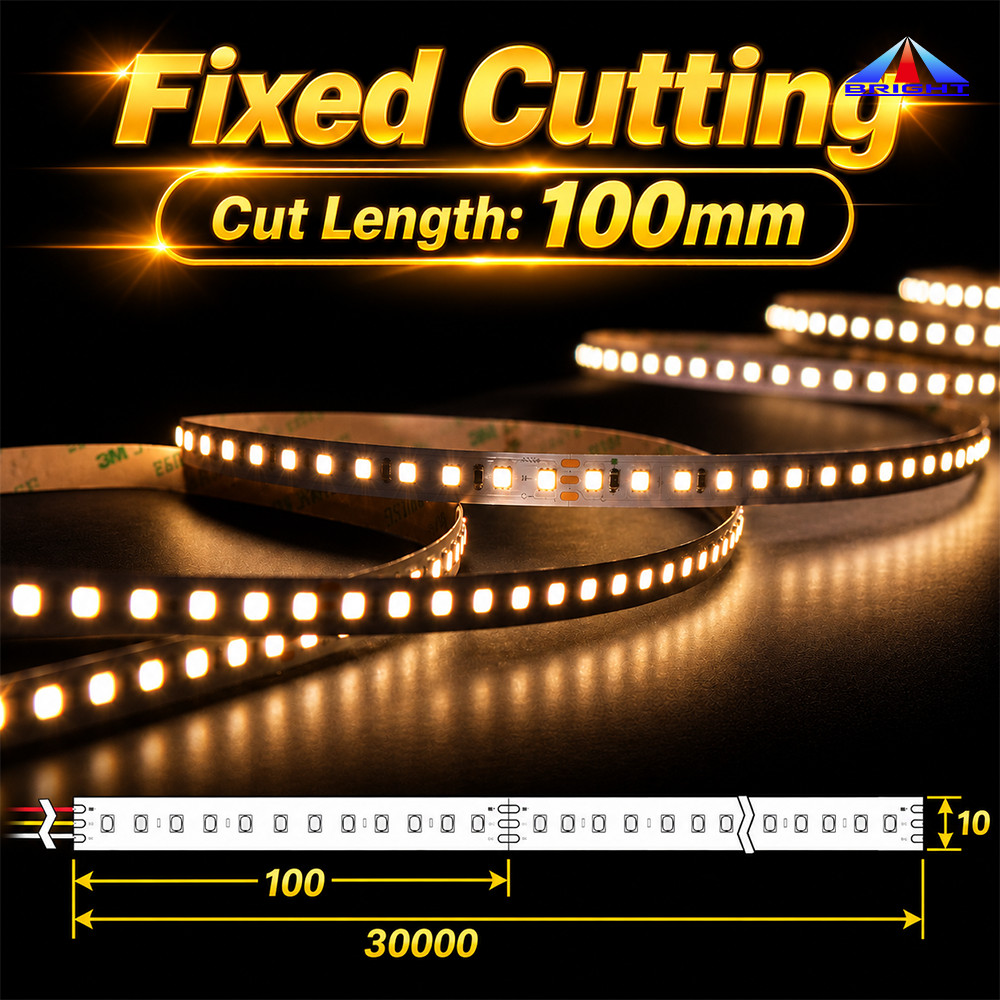
Commercial reception desks cut from backlit translucent granite or translucent acrylic matrices. Utilizing our DC48V long-run LED strips and 10M continuous ultra-slim sheets ensures steady brightness across 8-meter seamless counter runs without voltage drop or power feed breaks.
Luxury Residential Kitchen Islands (Belén & San Rafael)
High-end residential villas in Heredia demand backlit kitchen islands and wet bars. Our cuttable DC24V CCT light sheets fit precisely underneath complex stone cutouts for sinks and cooktops, providing water-protected (IP54/IP65) illumination under 30mm thick stone tops.
Boutique Hotel Accent Feature Walls & Wellness Spas
Full-wall backlit onyx features in luxury boutique hotel lobbies create breathtaking organic art pieces. Coupled with DMX512 or WiFi/Zigbee smart controllers, property operators can program subtle dynamic light scenes matching local events or time-of-day moods.
High-End Retail Display Cases & Jewelry Showrooms
Retail stores in Heredia’s major commercial centers require flicker-free, zero-UV backlighting for luxury handbag and watch displays. Our ultra-thin light sheets emit zero infrared/UV radiation, preventing heat damage or discoloration to delicate retail merchandise.
Market Trends: Sustainable Green Luxury & Energy Decarbonization in Costa Rica
Costa Rica is world-renowned for its commitment to environmental sustainability, operating on nearly 99% renewable electricity. Consequently, commercial developers and municipal planners in Heredia insist on ultra-high luminous efficiency (lm/W) to meet rigorous green building standards, such as LEED Gold and Costa Rica’s national Bandera Azul Ecológica certification for sustainable construction.
Traditional backlight box systems used fluorescent tubes or inefficient high-wattage modules, burning over 150W per square meter and generating excessive ambient heat. Shenzhen Covek Lighting’s next-generation backlight sheets deliver up to 140 lumens per watt using state-of-the-art Flip-Chip LED technology. By reducing energy consumption to just 36W-48W per square meter while yielding superior surface lux, our lighting solutions align perfectly with Costa Rica’s decarbonization goals and lower long-term operating expenditures for commercial operators in Heredia.
Why Leading Heredia Importers & Fabricators Partner with Covek Lighting
Founded in 2011 in Shenzhen’s Longhua District, Shenzhen Covek Lighting Co., Ltd. operates a 5,175 m² manufacturing center equipped with automated SMT production lines, high-precision FCOB encapsulation systems, and integrating sphere quality control suites. Audited onsite by TÜV Rheinland, we provide complete OEM/ODM solutions tailored for North American and Latin American markets.
Heredia Local Procurement & Engineering FAQ
Clear, technical answers to common questions asked by stone fabricators, electrical engineers, and lighting buyers in Costa Rica.
How do Covek backlight panels handle Costa Rica’s 120V / 60Hz grid standards?
What thermal dissipation steps are required behind thick translucent marble in tropical microclimates?
Can local Heredia stone fabricators cut and shape the LED sheets directly on-site?
Which IP rating should be specified for high-humidity installations in Heredia and coastal Costa Rica?
What are the freight options, customs documentation, and delivery timelines to Costa Rica?
Why is CRI > 90/95 crucial when backlighting imported translucent quartzite and onyx?
Request Custom Backlight Samples & Technical Engineering Support for Heredia Projects
Planning an upcoming commercial lobby, luxury kitchen island, or hotel accent wall in Heredia or the Central Valley? Our technical lighting engineers are ready to calculate your optical depth ratios, recommend light sheet specifications, and provide factory-direct wholesale quotes.
Contact Us