Precision-Engineered Waterproof LED Lighting Portfolio
Delivering factory-direct OEM/ODM solutions tailored for architectural, commercial, and high-moisture applications. Compliant with international CE, RoHS, UL, and EMC standards.
Architectural Engineering Whitepaper: Waterproof LED Strip Metallurgy, Polymer Chemistry, and Thermal Dynamics
As commercial lighting design advances toward integrated seamless illumination, the demand for high-reliability waterproof LED strips, Flip-Chip COB (FCOB) modules, and cuttable backlight sheets has transitioned from decorative accenting to structural architectural elements. Selecting an OEM/ODM supplier requires rigorous technical evaluation of physical material science, thermal dissipation efficiency, optical color consistency, and long-term ingress protection performance under harsh environmental stress.
Modern architectural lighting projects—ranging from high-humidity indoor hospitality coves to exterior building facades exposed to UV radiation and thermal cycling—demand strict engineering parameters. A failure rate of less than 0.01% over a 50,000-hour lifespan is the baseline benchmark for professional procurement directors.
Extrusion Chemistry: Silicone vs. Epoxy
Traditional PVC and epoxy resin encapsulations suffer from rapid yellowing, brittleness under UV radiation, and thermal shrinkage. Premium OEM waterproof LED strips utilize food-grade optical silicone co-extrusion, retaining >95% light transmittance while operating from -40°C to +80°C with zero chemical degradation.
Copper Board Thickness & Thermal Paths
Voltage drop and thermal throttling are primary causes of premature lumen degradation. Sourcing architectural-grade strips demands 3oz/4oz dual-layer rolled copper flexible printed circuits (FPC), lowering internal impedance and ensuring uniform luminance across continuous 10-meter to 50-meter runs.
Ingress Protection: IP65 to IP68 Dynamics
Engineered waterproofing extends beyond simple surface spray coatings. IP67 and IP68 ratings are achieved via solid-state integrated silicone extrusion with nano-hydrophobic interior sealing, preventing capillary water moisture ingress through thermal contraction cycles.
Technological Evolution Trends in Industrial & Architectural LED Lighting
The global LED strip market is undergoing a structural transition driven by advancements in semiconductor packaging, optical efficiency, and micro-controller integration. Engineering teams and procurement managers must align their 3-to-5-year product roadmaps with key technology vectors:
1. Flip-Chip COB (FCOB) Seamless Lighting Arrays
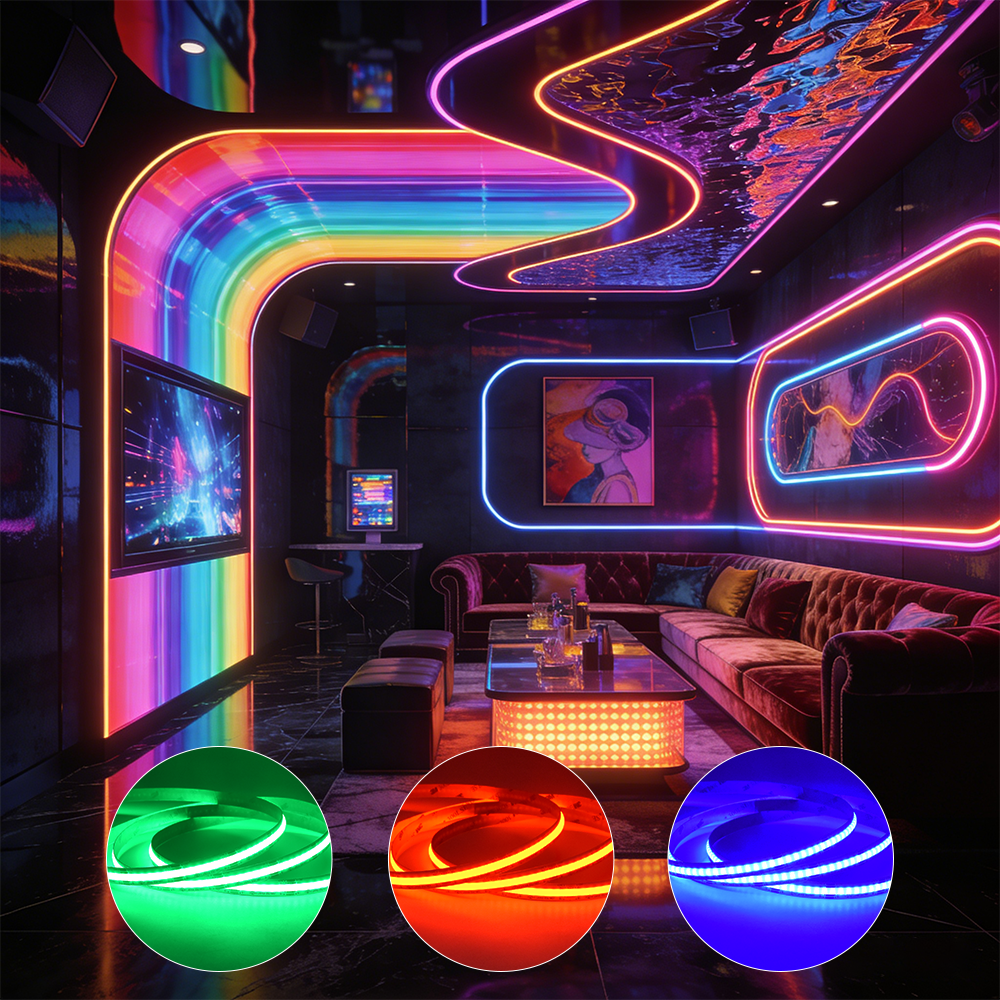
Conventional Surface Mount Device (SMD) LED tapes rely on discrete packaged diodes, often producing visible "hotspots" or requiring deep aluminum extrusion profiles with heavy frosted diffusers. FCOB technology directly bonds flip-chips to the FPC board using continuous phosphor coating layer application. With die densities exceeding 528 to 840 chips per meter, FCOB strips eliminate pixelation entirely while reducing profile height requirements to less than 2mm.
2. Ultra-Long Voltage-Drop Mitigation Architectures (DC48V)
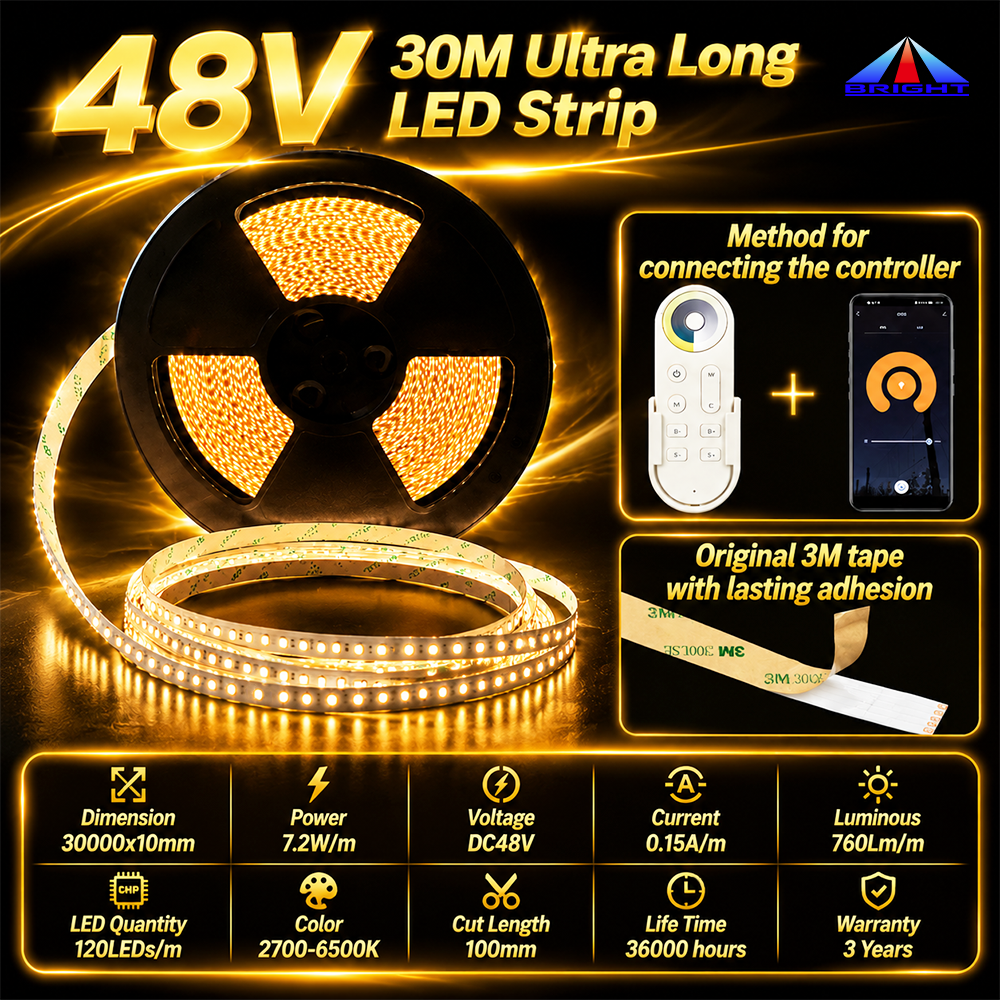
High-power architectural installations previously required complex wiring, frequent power feeds, and bulky power supplies to counter DC24V attenuation over distance. The industry shift toward DC48V constant-current strip architectures cuts operating current by 50%, enabling continuous single-ended runs up to 30 meters with less than 3% luminance variance from driver to tail.
3. Cuttable Matrix Backlighting Sheets for Translucent Stone & Acrylic
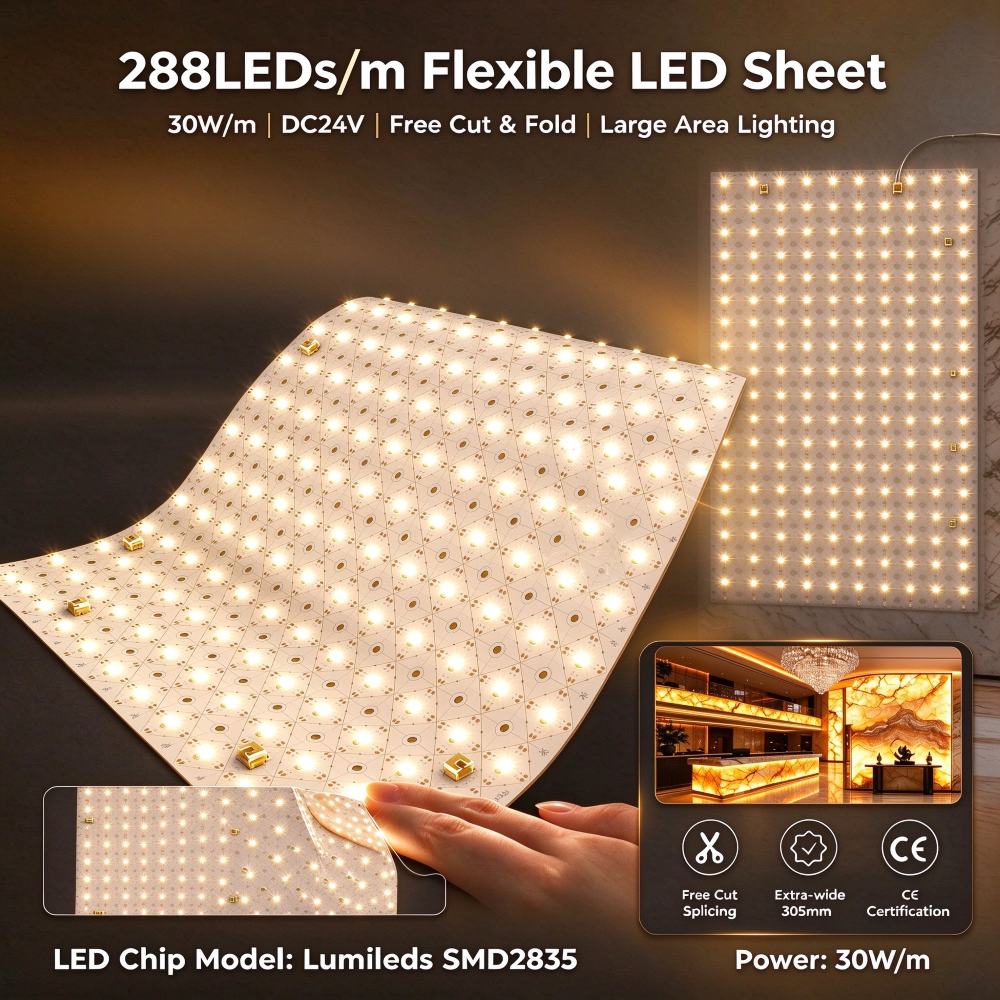
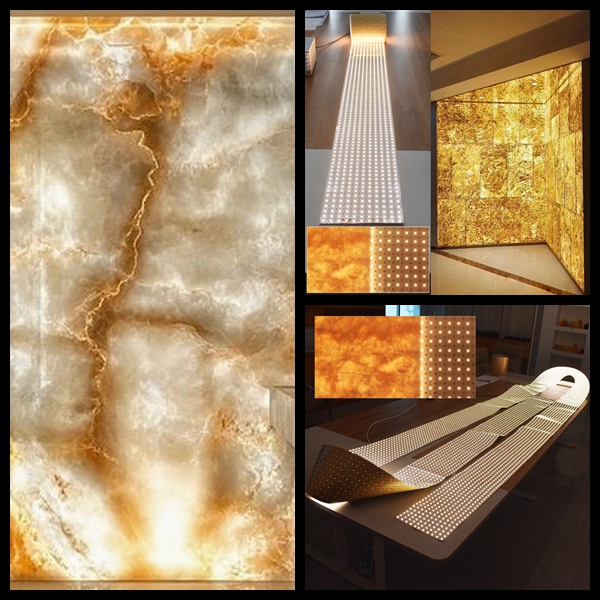
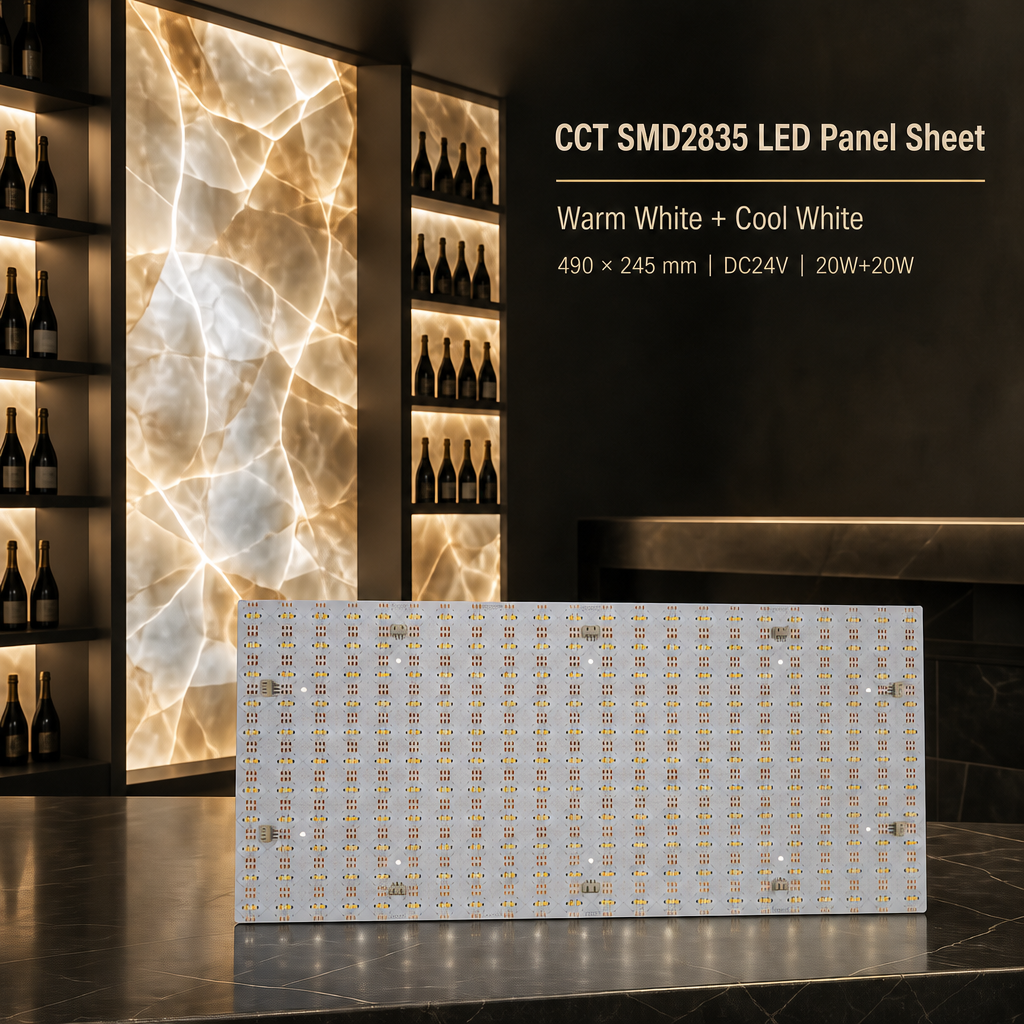
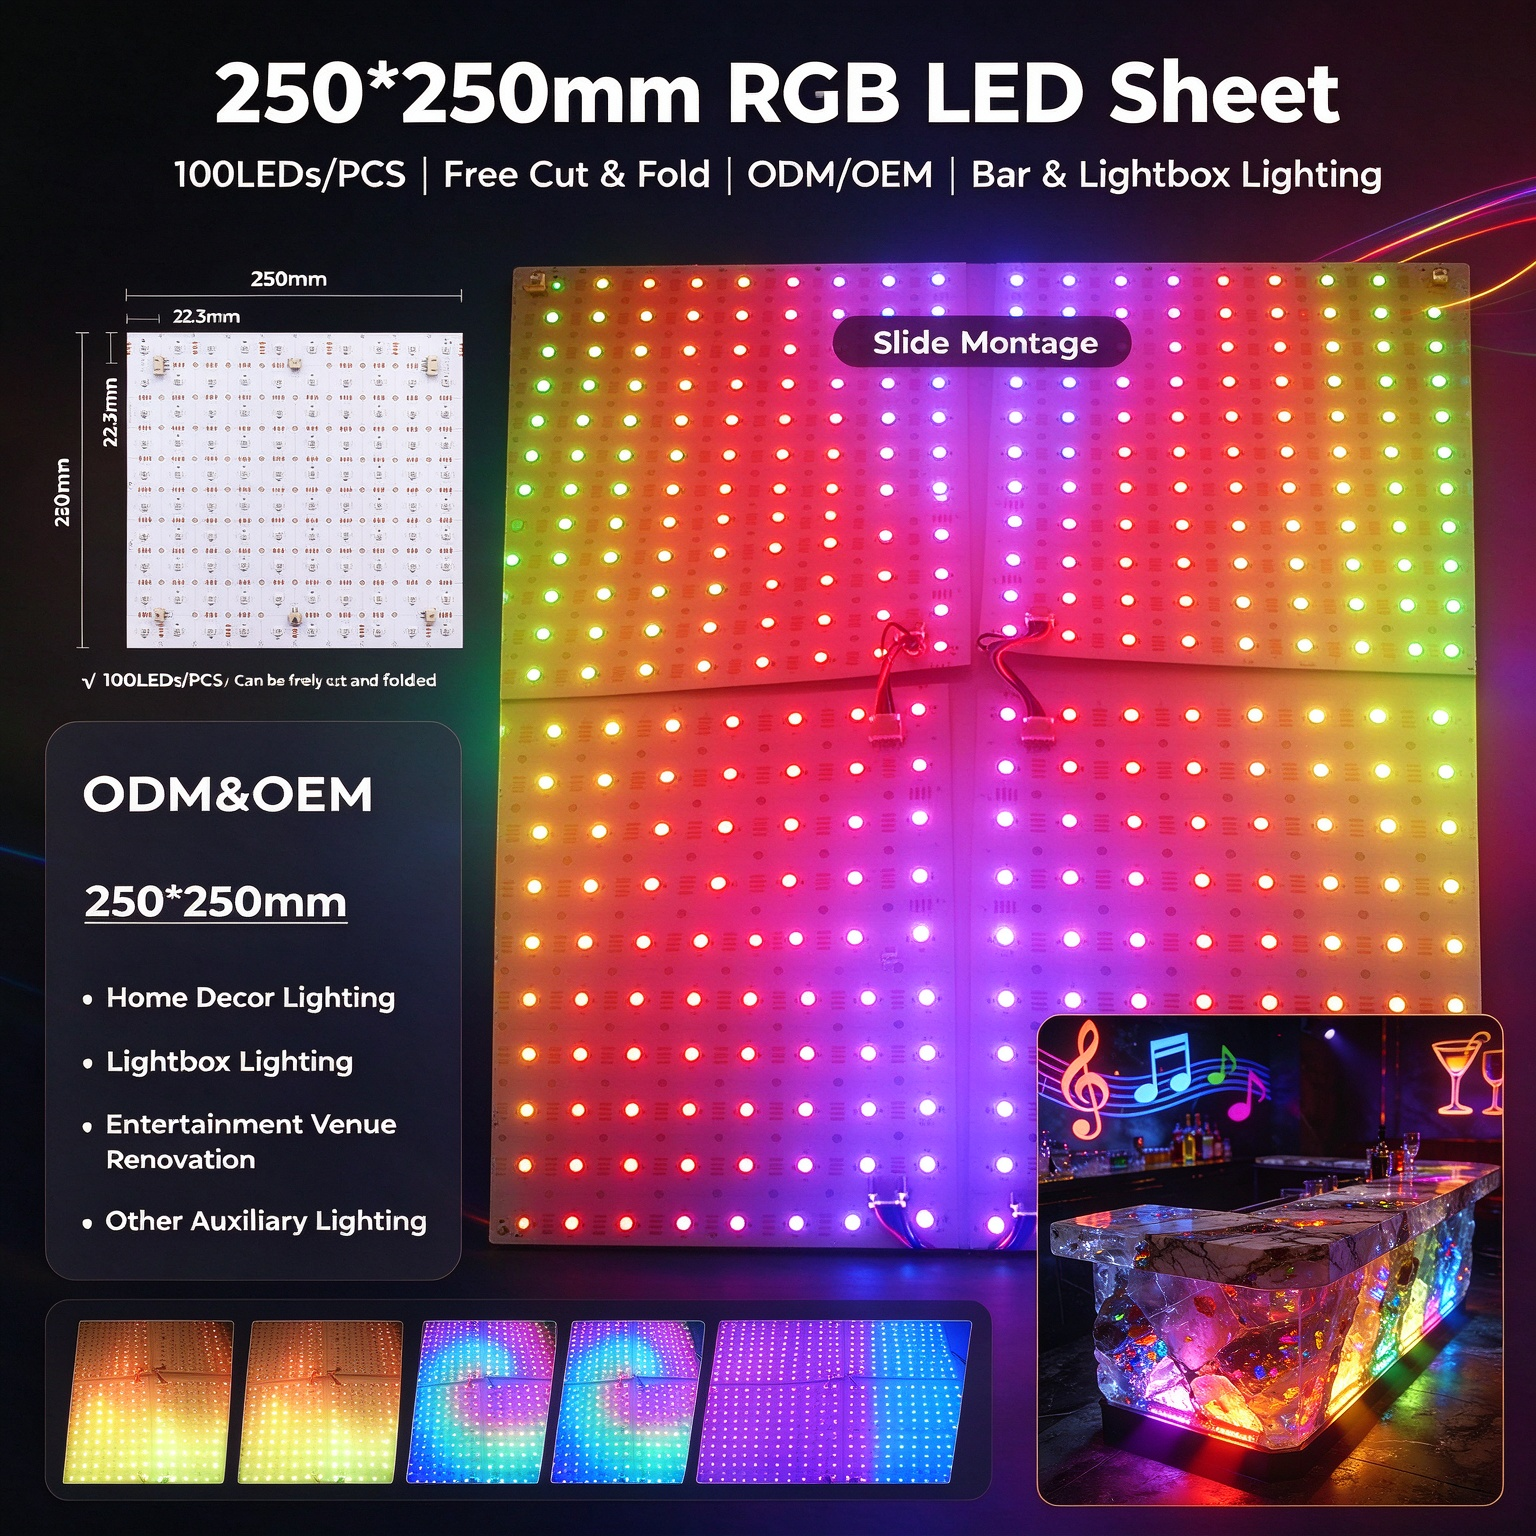
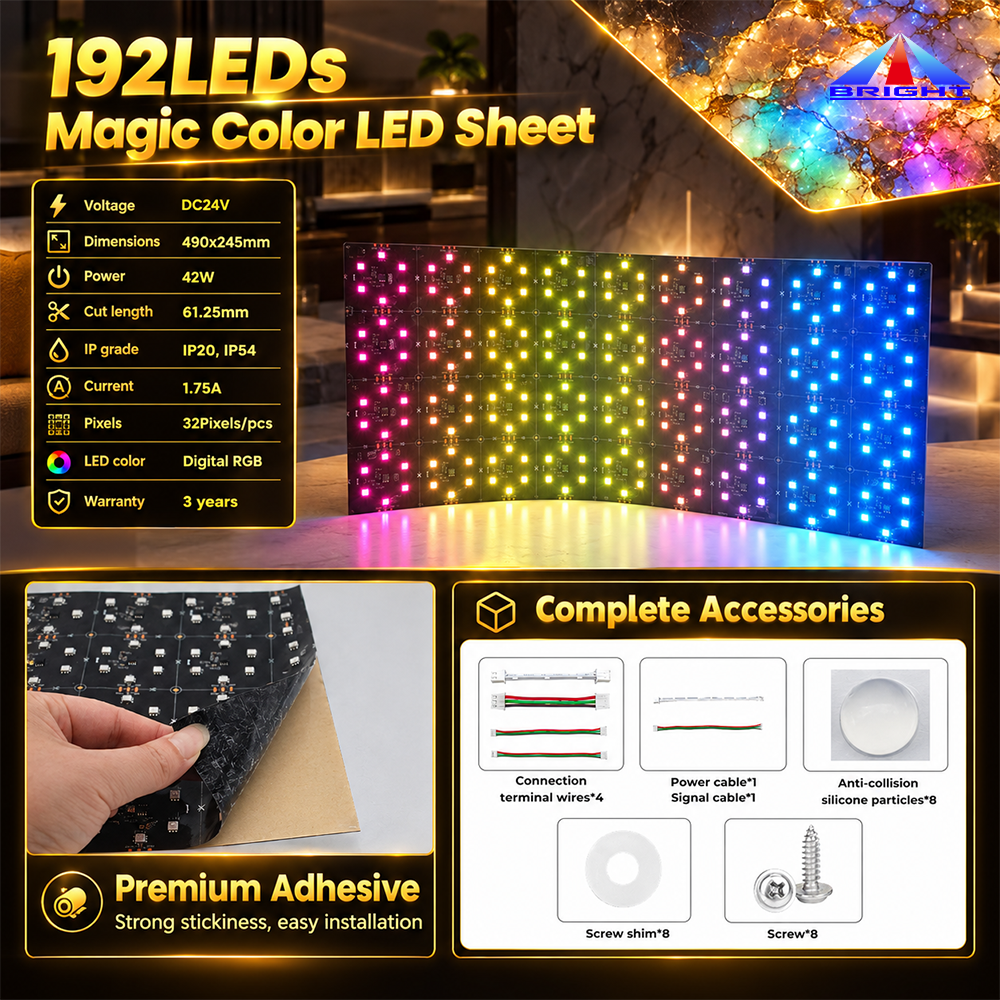
Custom stone fabricators and backlit display builders historically struggled with rigid LED tiles or non-uniform edge lighting. Flexible, modular cuttable LED sheets (such as 610x305mm matrix panels) feature grid-pattern cut points every single LED chip. This allows installers to trim sheets around complex organic curves, plumbing cutouts, and custom wall geometries without soldering or dark spots.
Global Sourcing & Procurement Trends for Waterproof LED Strips (2025–2030)
As global supply chains demand greater transparency, sustainability, and compliance, international buyers are shifting their vendor selection criteria. Low unit cost is no longer the single decisive factor; total cost of ownership (TCO), regulatory compliance, and rapid ODM engineering capabilities now dictate supplier selection.
Demands for high color fidelity (CRI >95, TM-30 Rf>93, Rg>100) are standard across retail and luxury residential spaces.
Submersible chlorine- and saline-resistant silicone extrusion is replacing glass-filled lighting channels in marine environments.
Integration of SPI, DMX512, and wireless Matter/Zigbee connectivity directly onto smart addressable strip IC chips.
Strict single-binning guarantees batch-to-batch color temperature consistency across multi-phase global building projects.
Manufacturing Excellence & OEM/ODM Capabilities
Founded in 2011 in Longhua District, Shenzhen, Shenzhen Covek Lighting Co., Ltd. operates as a verified tier-one OEM/ODM manufacturer specializing in high-performance flexible lighting products. Operating a modern 5,175 m² factory with 133 skilled technical employees, Covek provides end-to-end manufacturing integrity backed by independent third-party audits.
TÜV Rheinland Verified Facility
Our manufacturing lines, management protocols, production capacity, and export credits are verified onsite by TÜV Rheinland. We ensure full transparency for international importers and distributors.
Integrated R&D & Customization
Releasing 20 to 50 innovative new products each month, our R&D team supports full PCB circuit design, custom silicone profile extrusion molding, specialized CCT binning, and private label OEM packaging.
Rigorous Quality Assurance
100% of finished orders undergo 24-hour burn-in testing, integrating sphere spectral checks, dynamic flex tests, and waterproof pressure immersion tests before export packaging under ISO 9001 quality systems.
Covek products carry full CE, RoHS, EMC, UL, ERP, and BIS documentation. With an annual export volume exceeding US$1.32 Million across North America, Western Europe, and Northern Europe, we offer flexible trade terms (FOB, EXW, Express) and payment methods including T/T, L/C, PayPal, and Western Union.
B2B Sourcing & Technical FAQ
Essential technical clarity addressing common procurement friction points for global lighting buyers.
Partner with a Trusted OEM/ODM Waterproof LED Manufacturer
Direct factory pricing, custom engineering support, free sample kits, and comprehensive compliance certificates for your next lighting project or product line launch.
Contact Us